Explore Our Liquid Ring Vacuum Pumps
Select a pump category based on the required suction capacity, vacuum level, process gas, available seal liquid, and operating conditions.

NASH liquid ring vacuum pumps are a reliable and durable solution for challenging process applications. Our liquid ring vacuum pump design was the first-of-its-kind at the turn of the 20th century and has been an industry leader ever since.
Through our ongoing commitment to innovation, product research, and development, Nash continues to introduce quality liquid ring vacuum pumps and product upgrades that meet the rigors of the most demanding applications while reducing the total cost of ownership.
Review our extensive product portfolio and discover the NASH liquid ring vacuum pump best suited for your process.
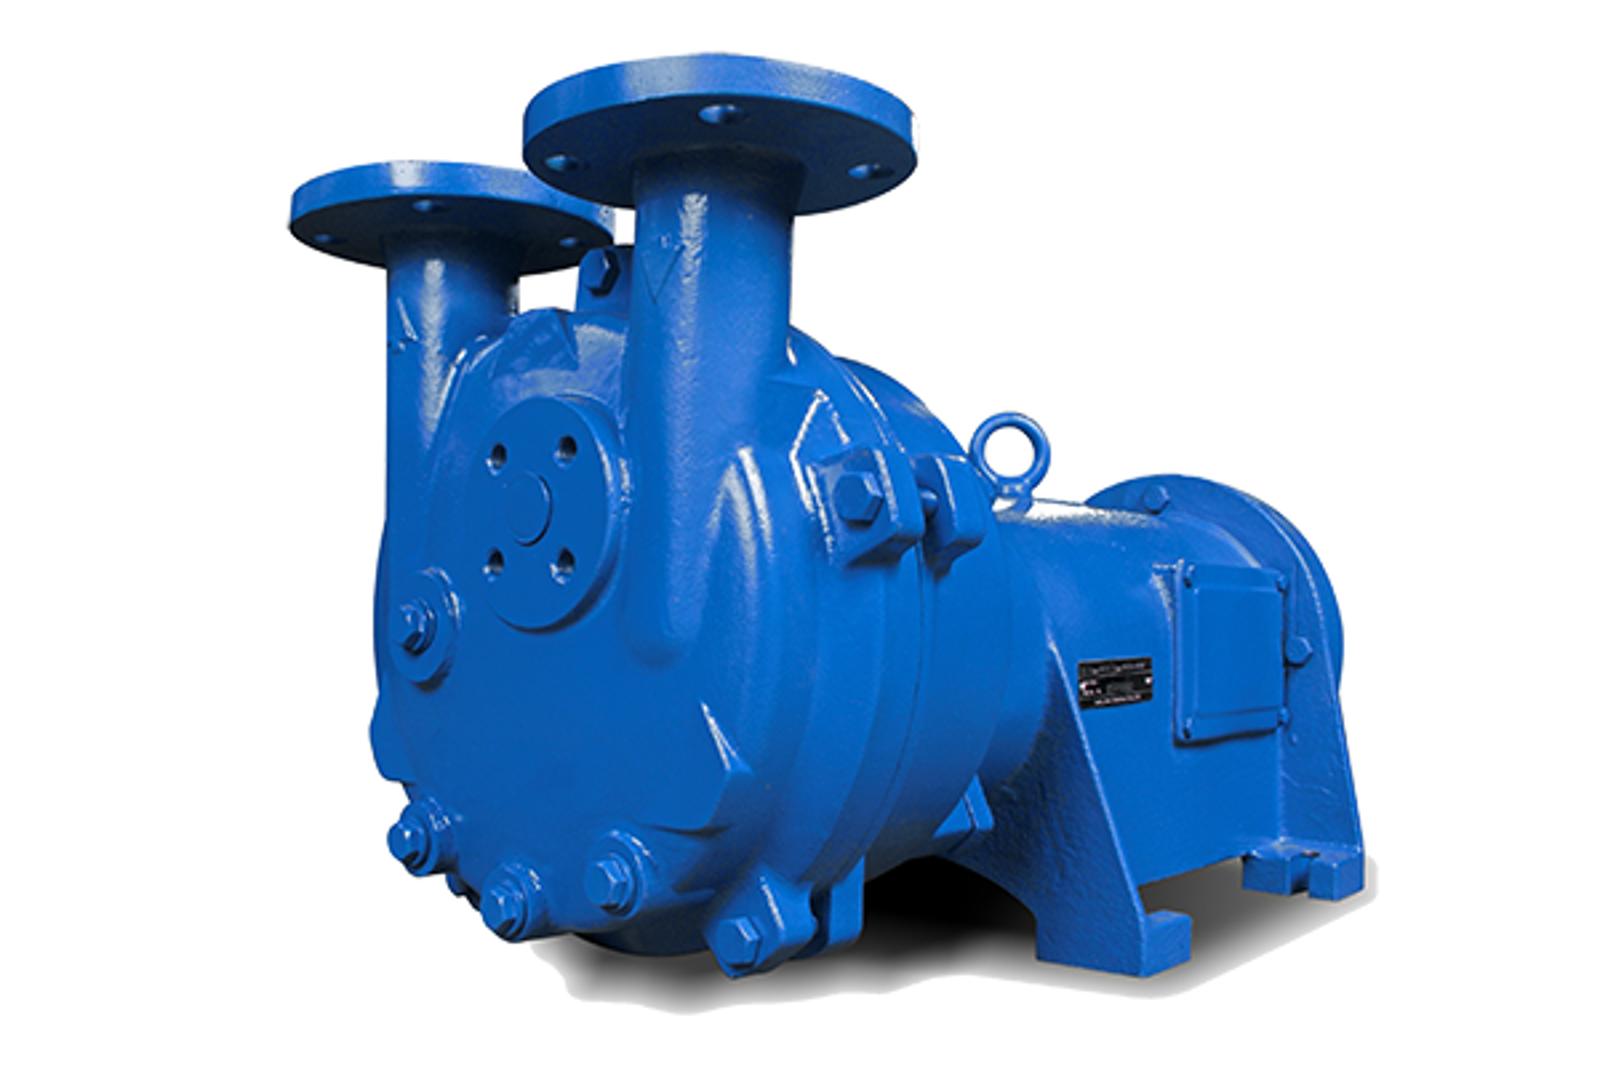
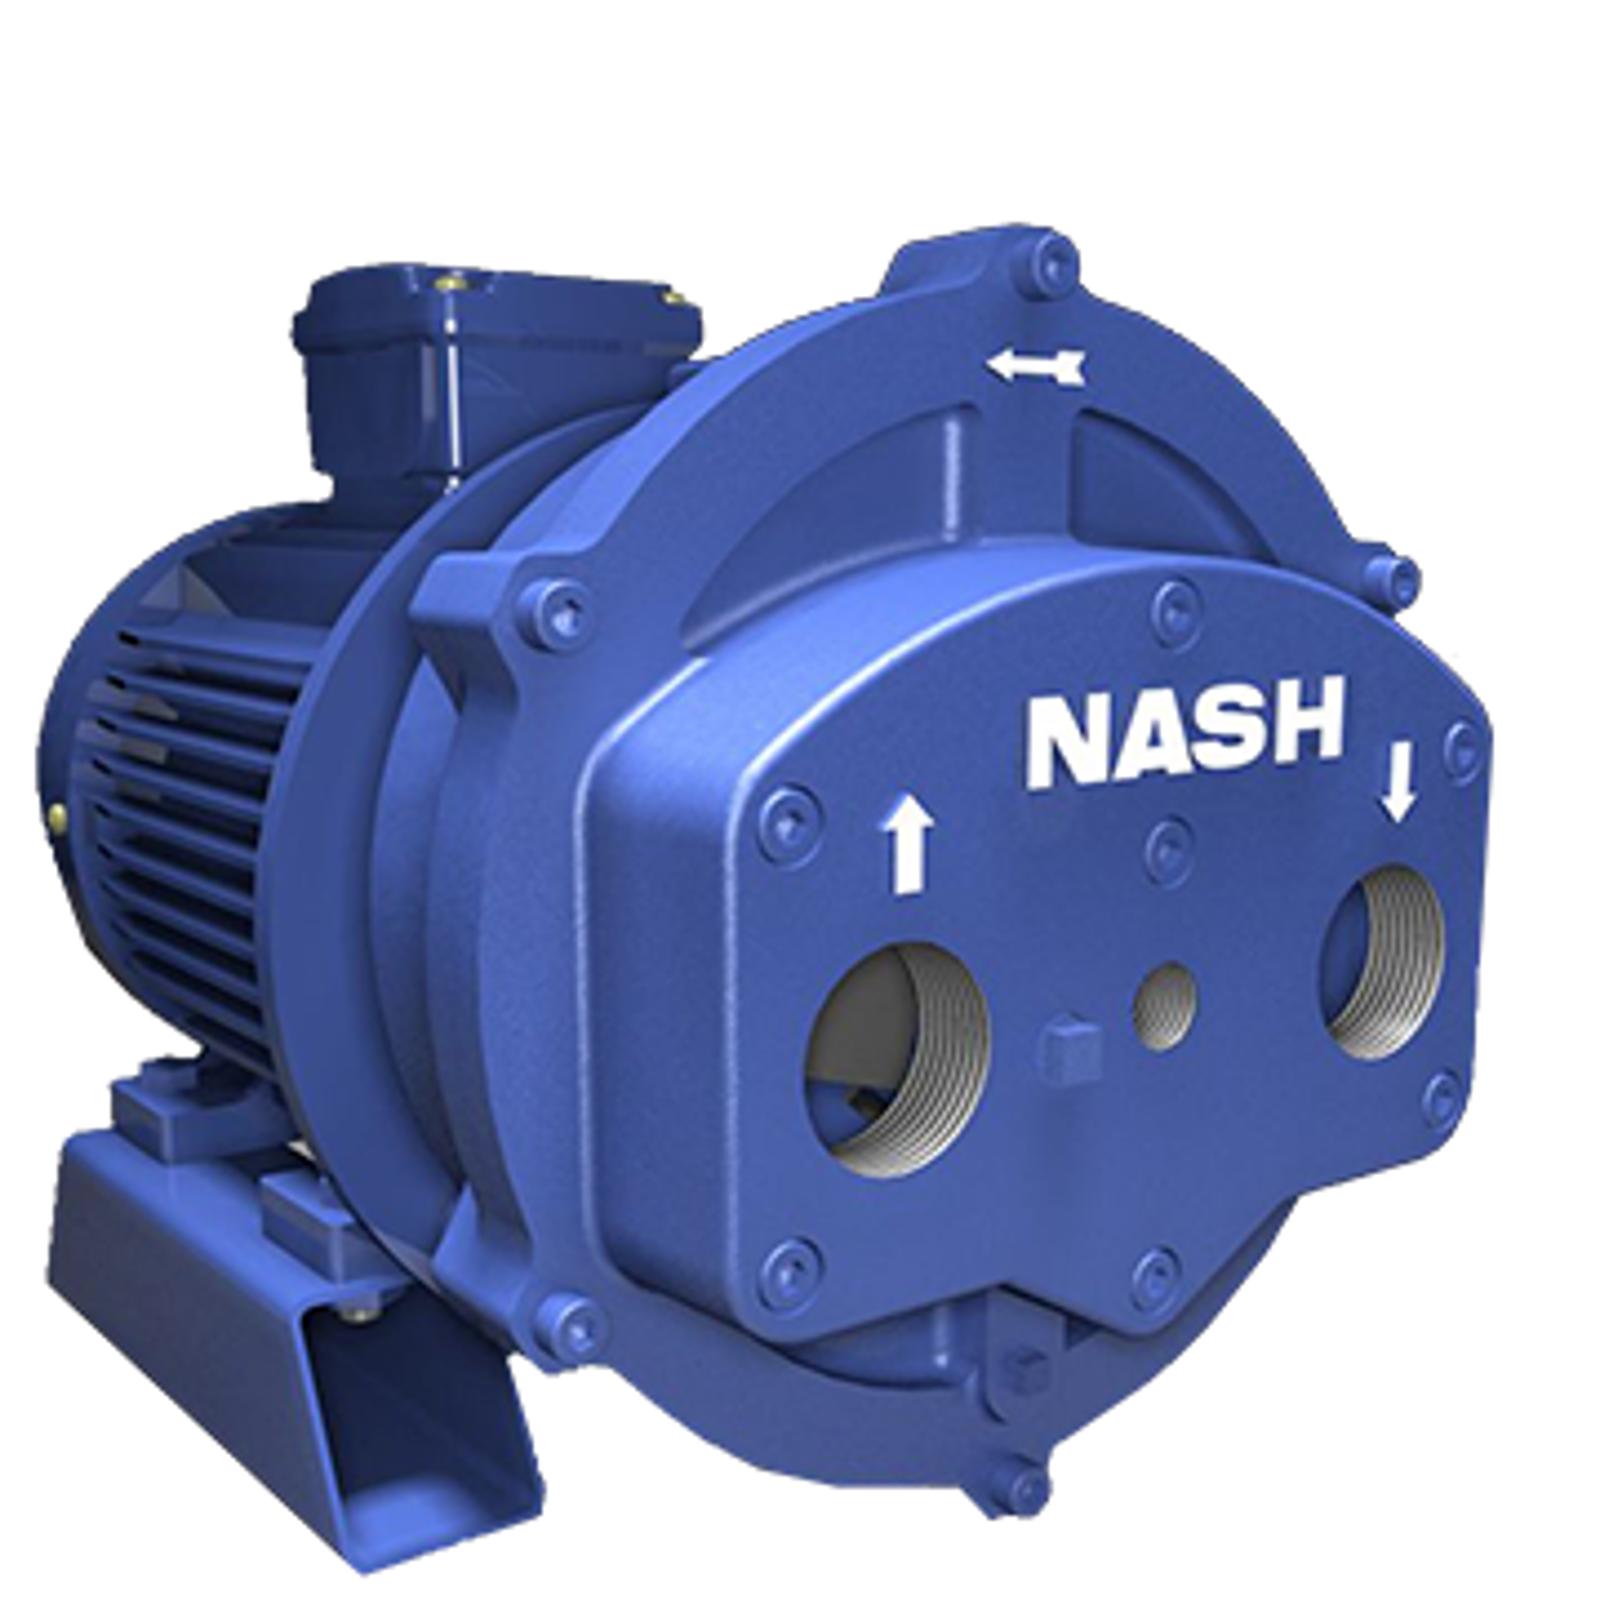
(Vacuum levels up to 29in. HgA, 1.5 HP to 10 HP)
NASH small capacity liquid ring vacuum pumps feature monoblock or lantern designs. These designs deliver the benefits of a simple, compact, and economical installation. Our small capacity liquid ring pumps are available in a variety of materials including cast iron and stainless steel and are ideal for use in a vast range of general industrial processes.
Click the link below to learn more about our small capacity liquid ring vacuum pumps.

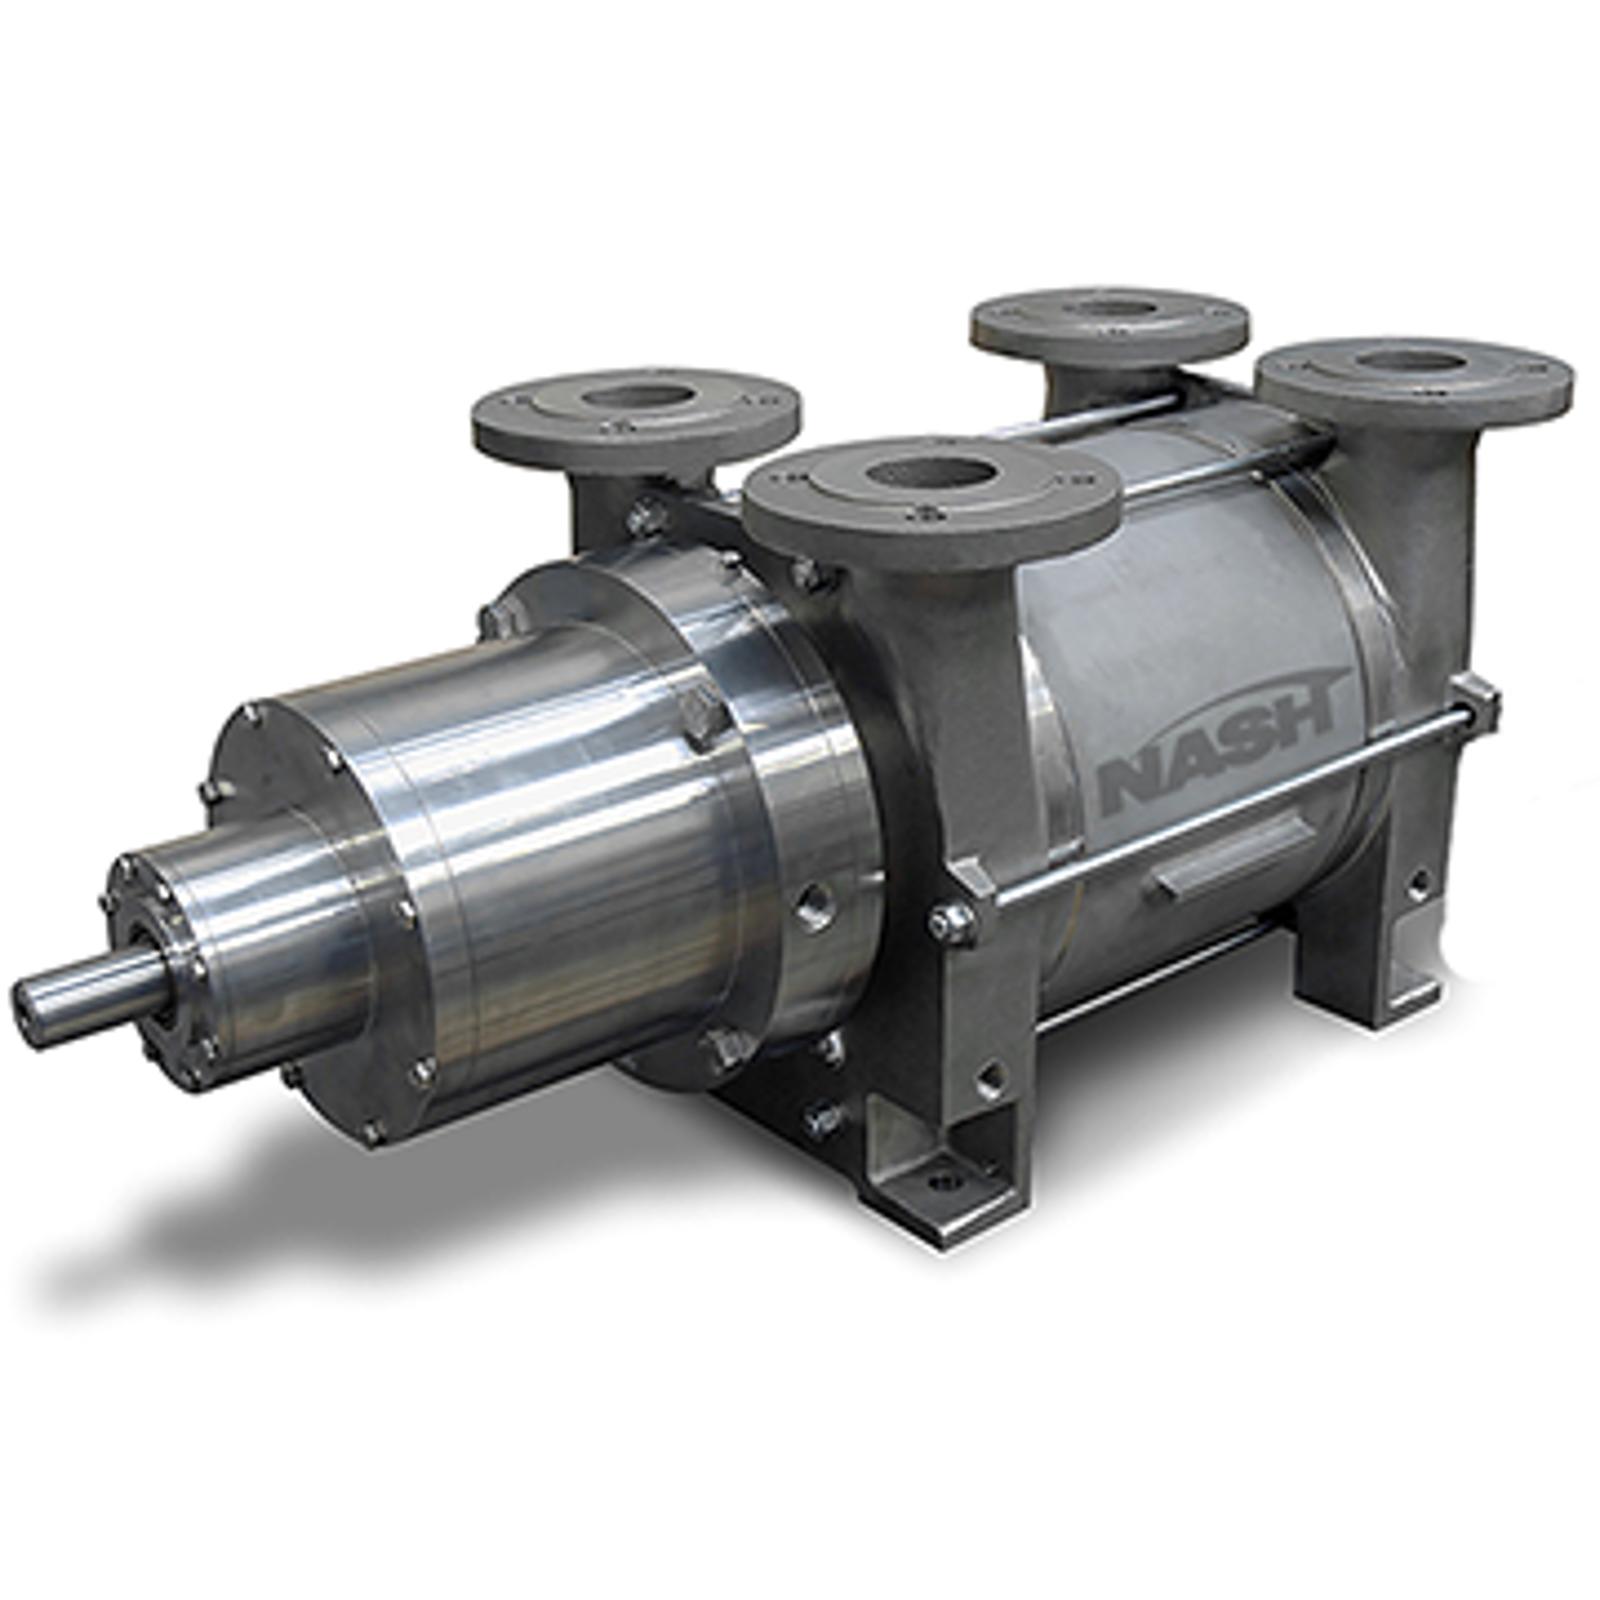
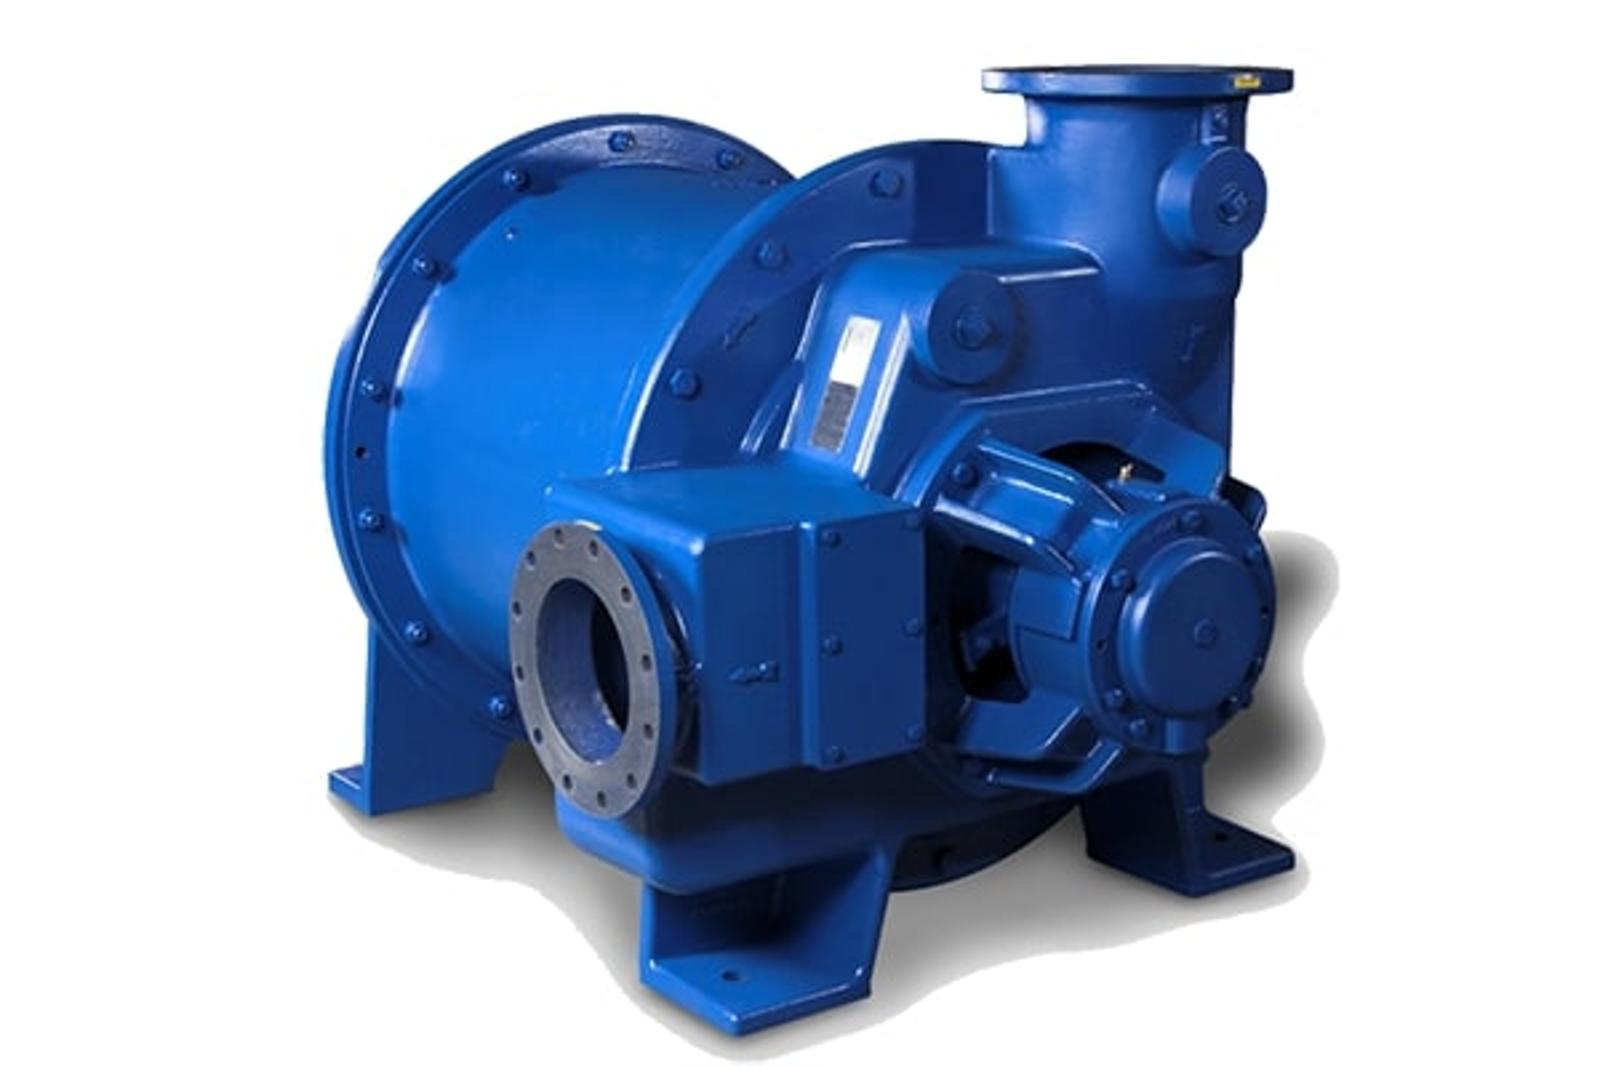
(Vacuum levels up to 28in. HgA, 10 HP to 200 HP)
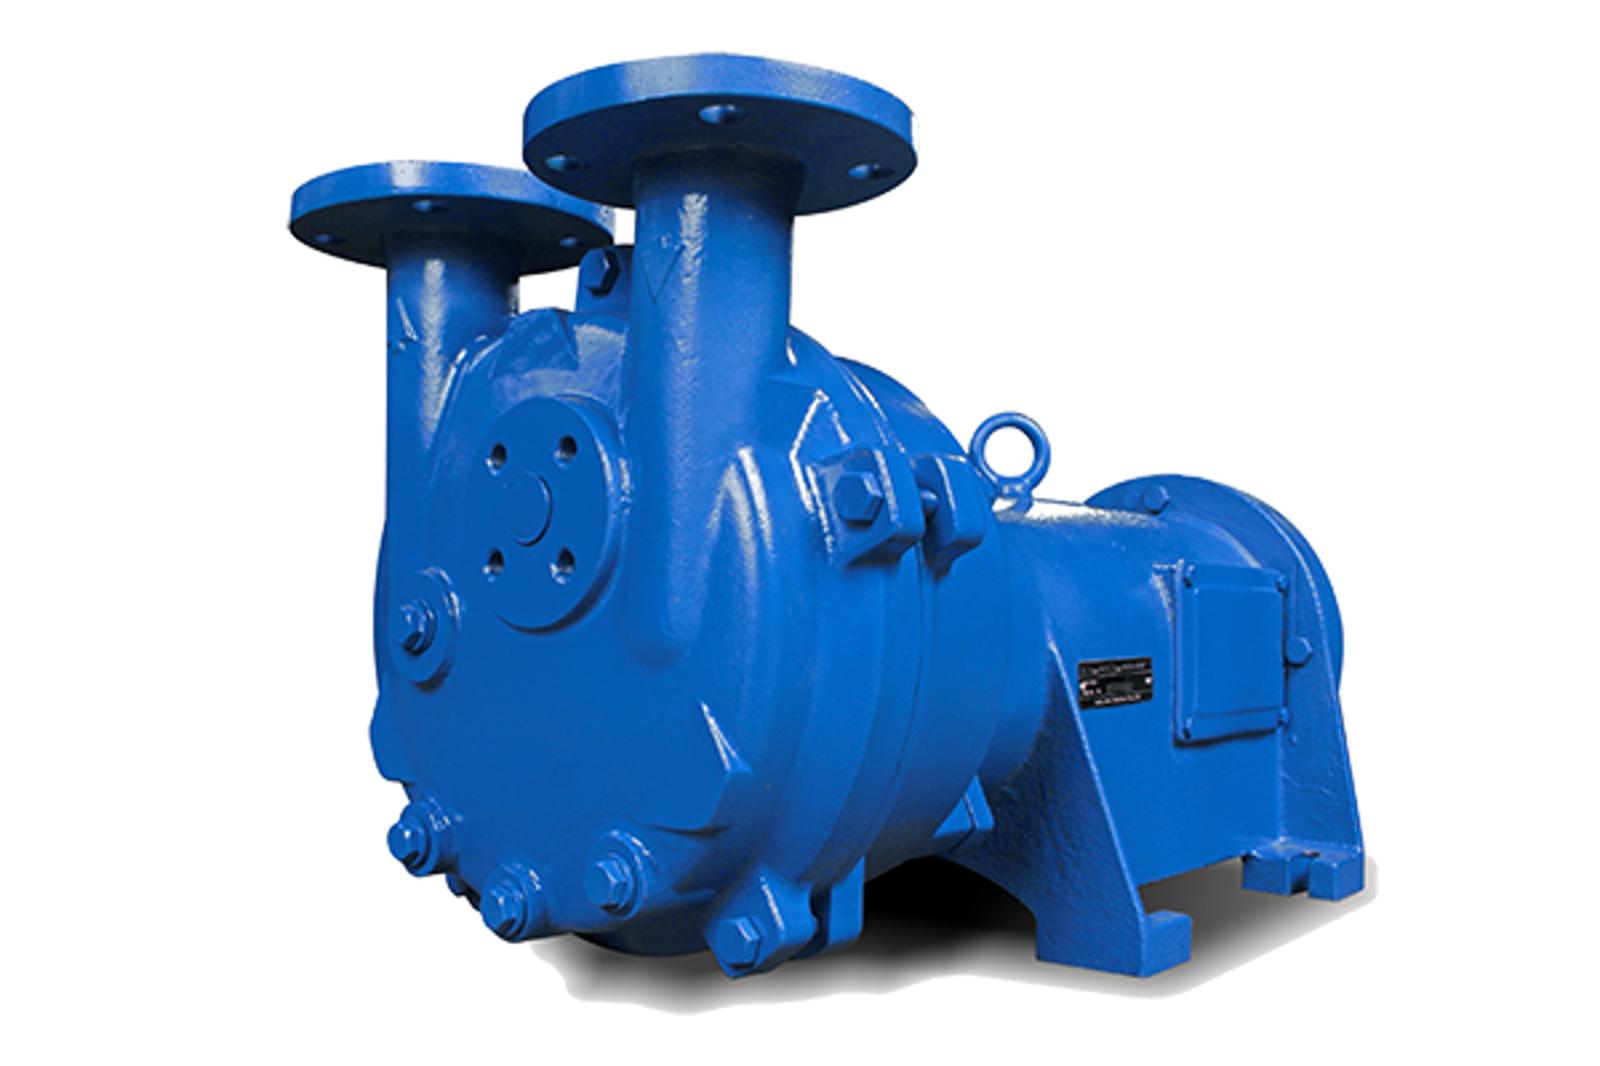
NASH medium capacity liquid ring vacuum pumps offer a highly powerful range of small to medium size single stage vacuum pumps for use in diverse industries including oil & gas, general industrial, and chemical.
Available in cast iron for less aggressive applications, and stainless steel for hostile applications and environments.
Click the link below to learn more about our medium capacity liquid ring vacuum pumps.
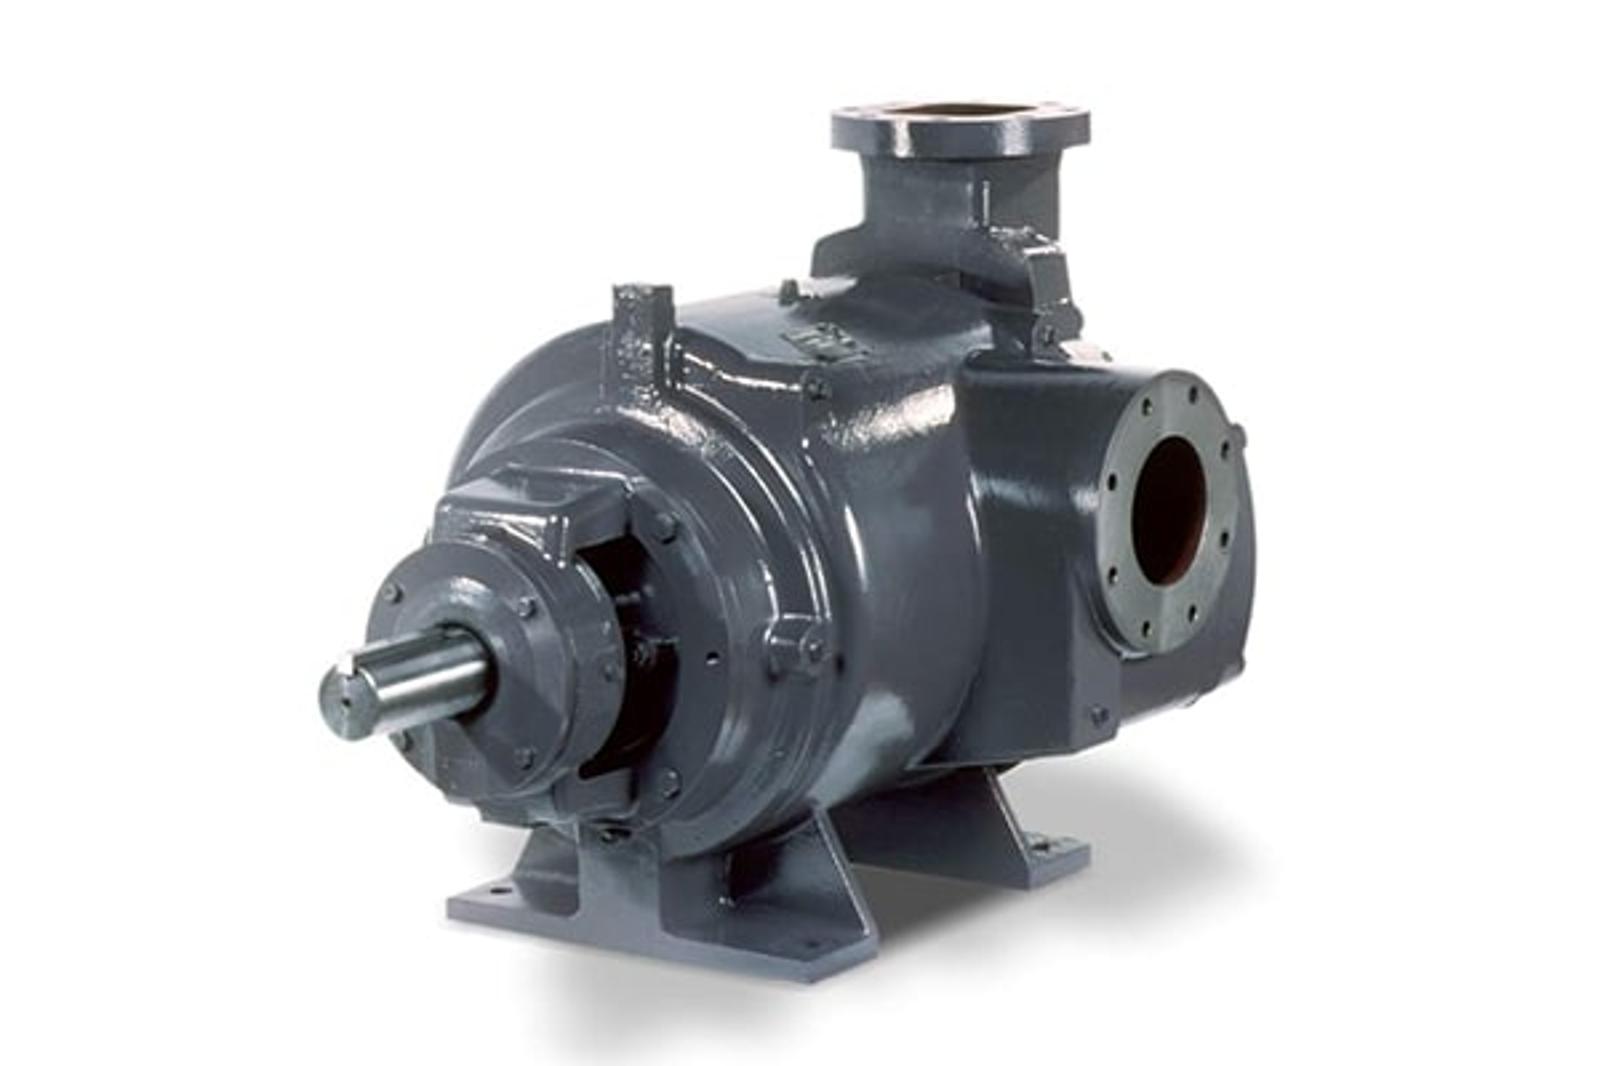


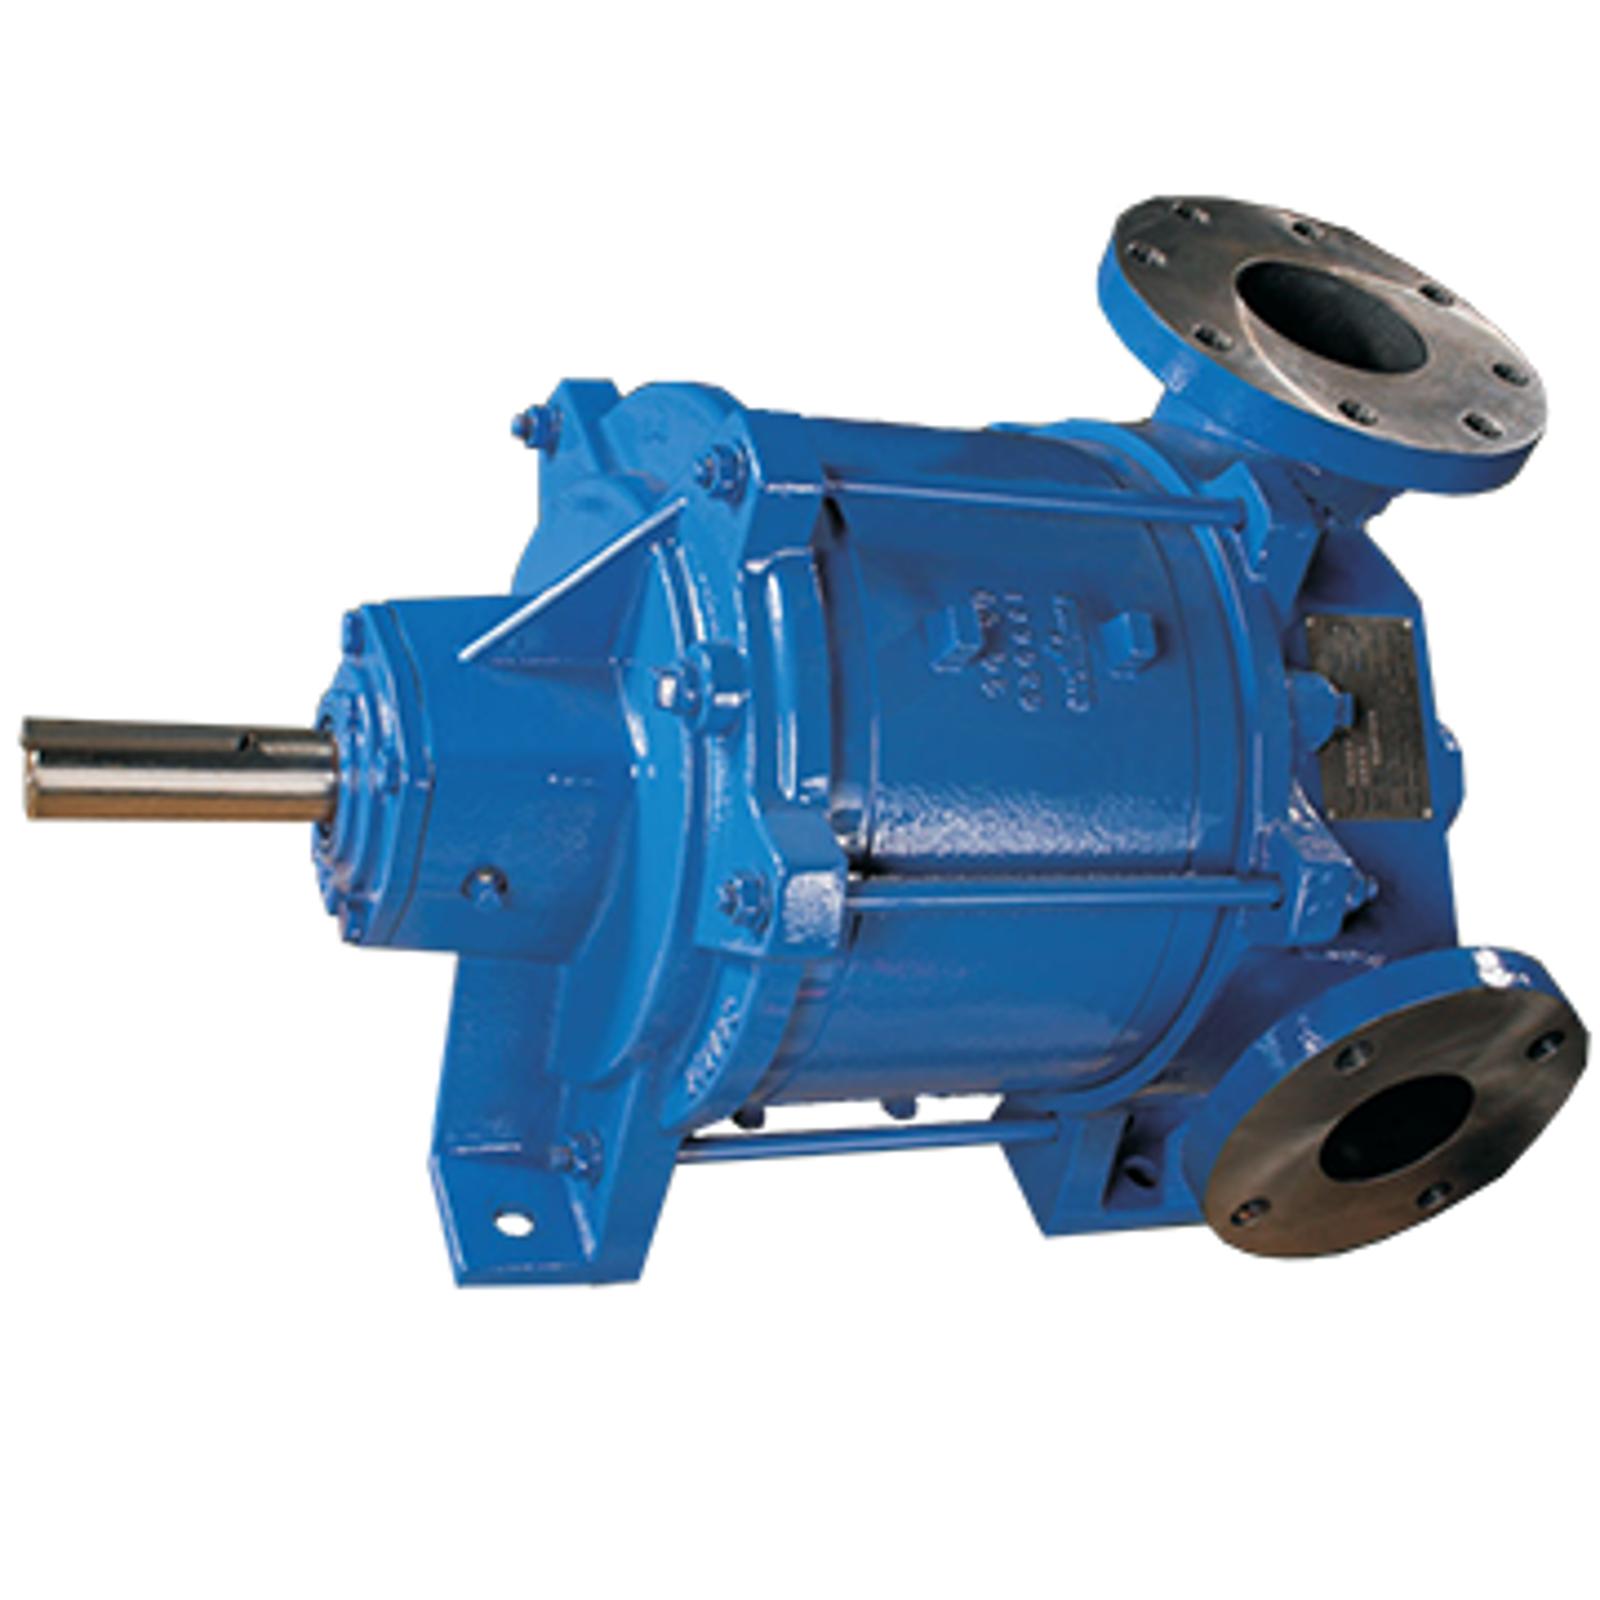
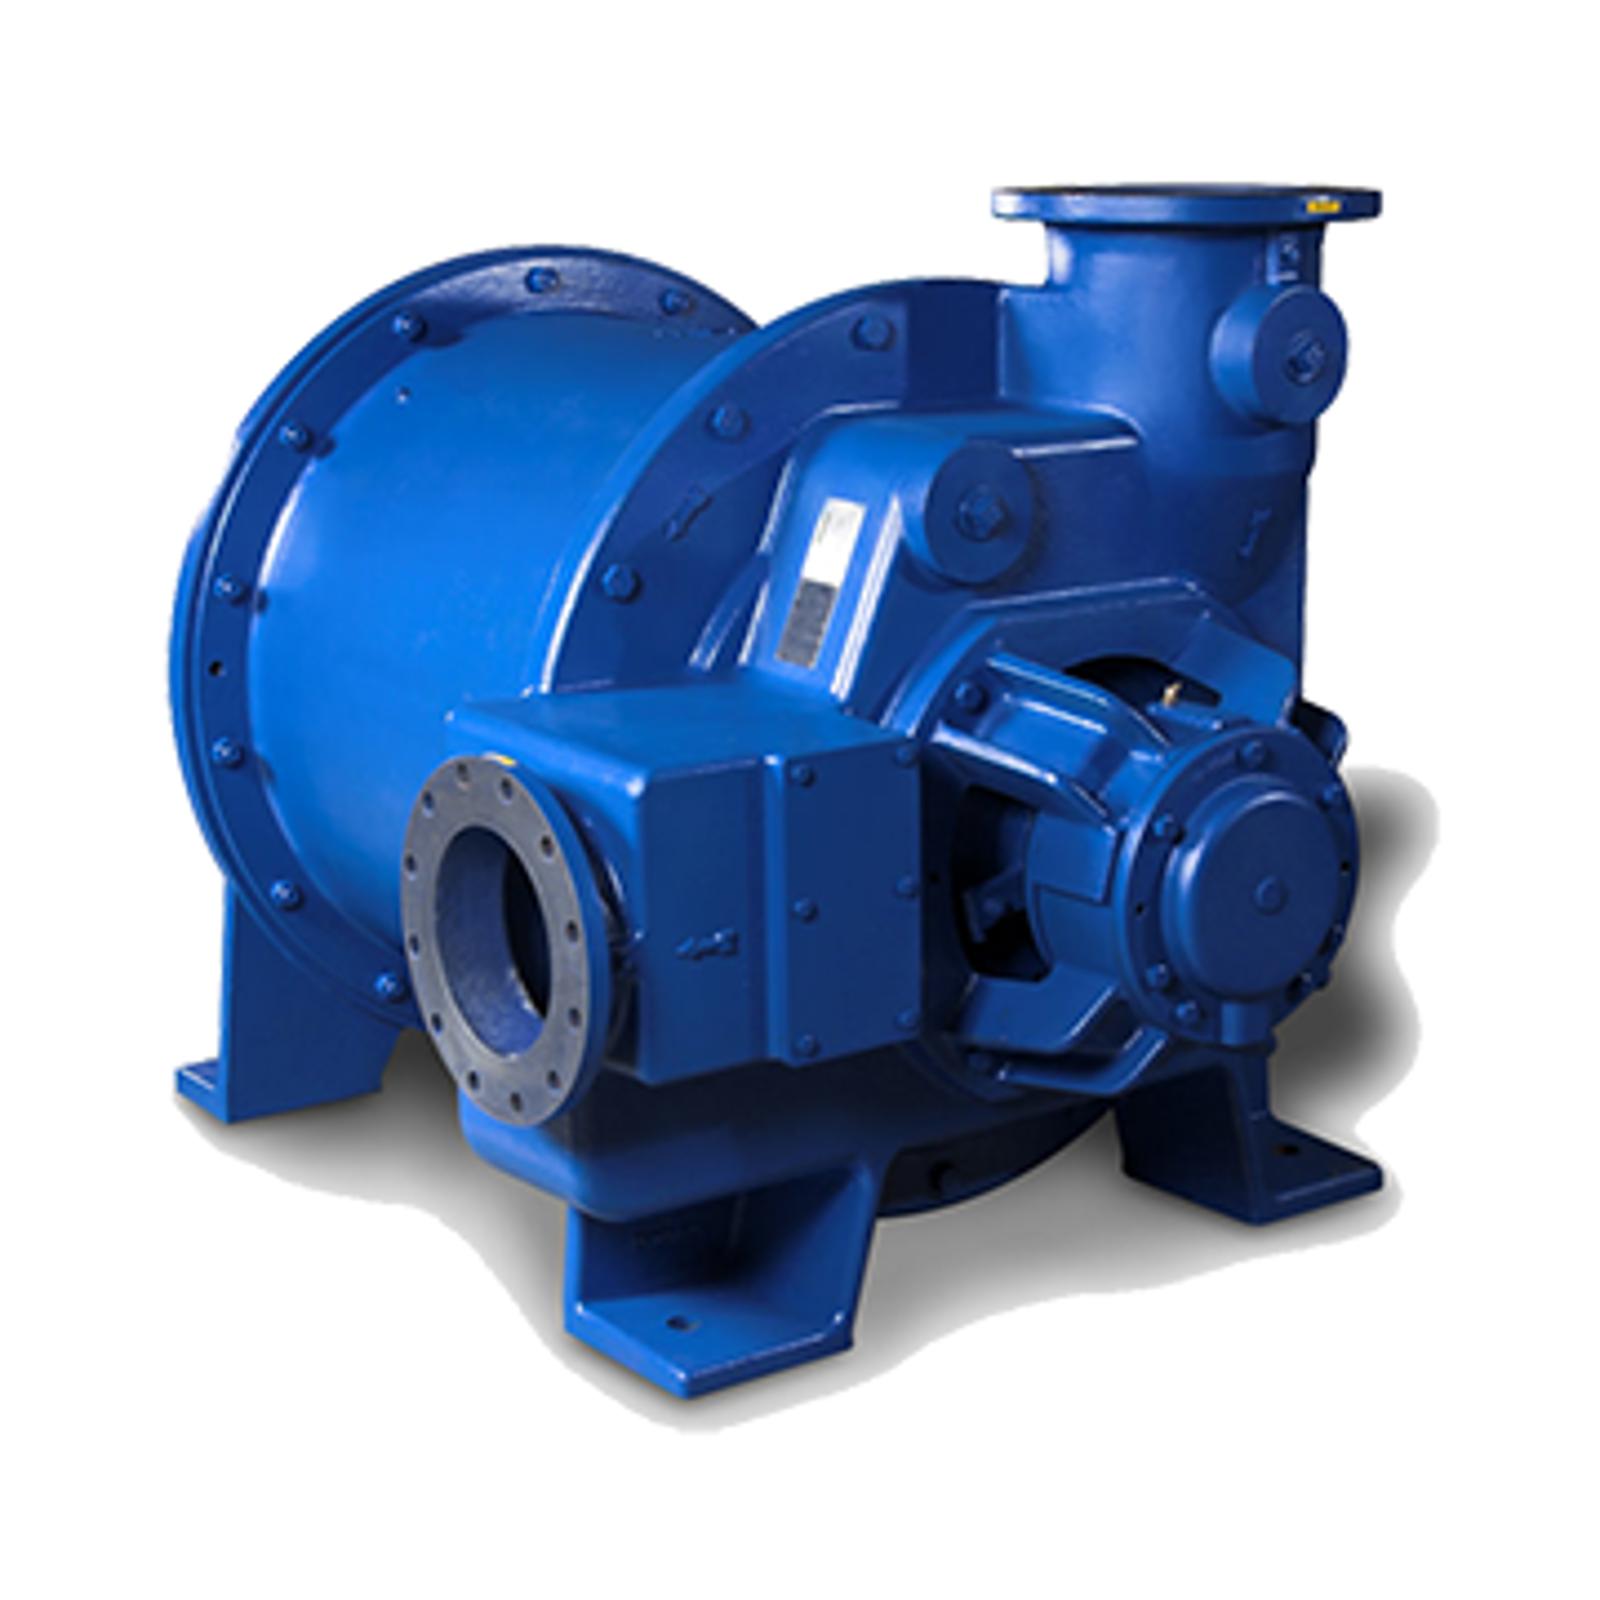
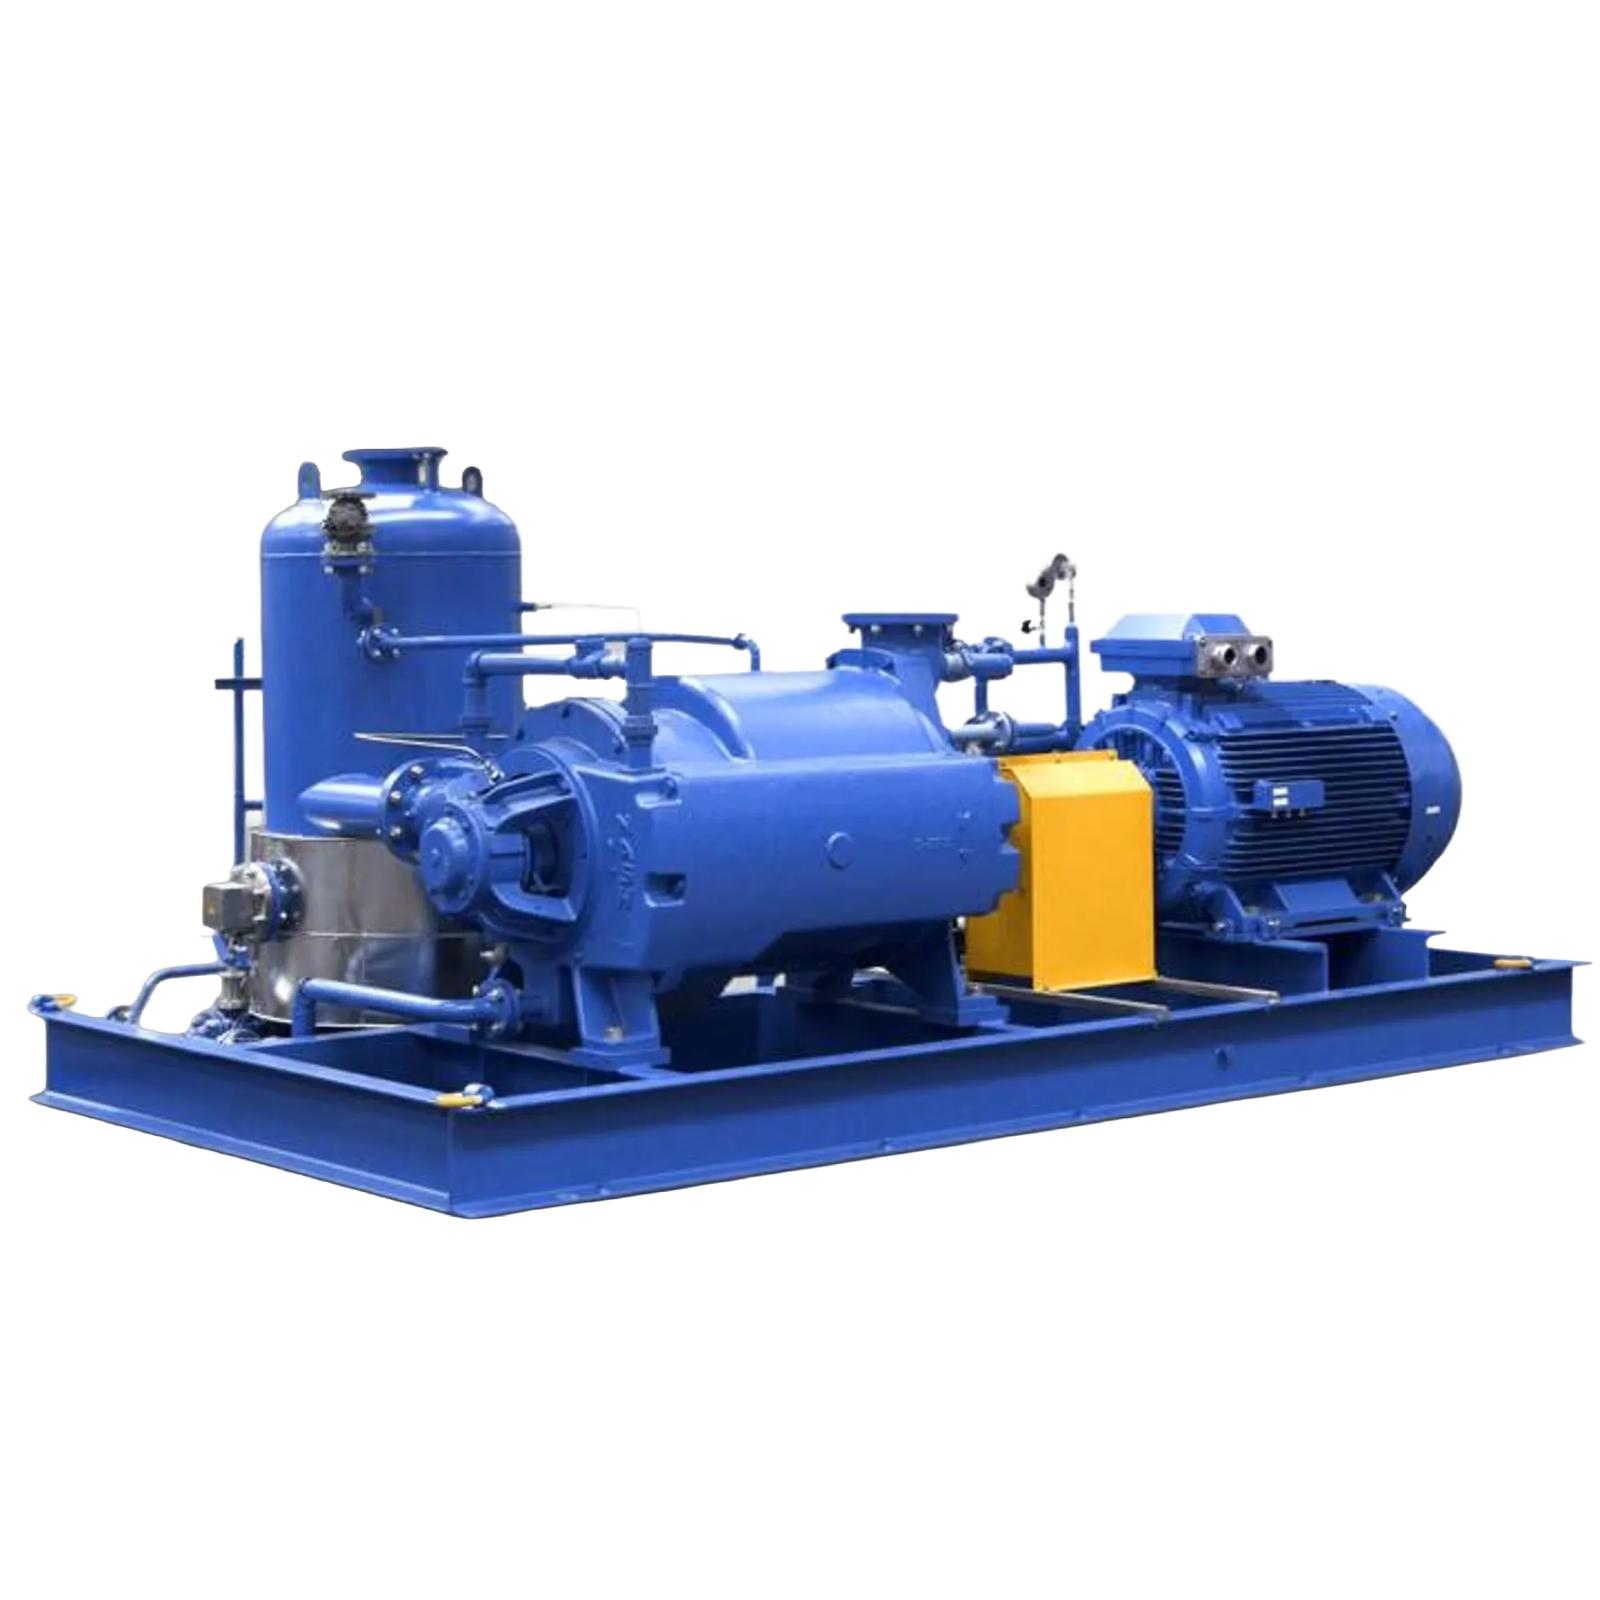
(Vacuum levels up to 25in. HgA, above 200 HP)
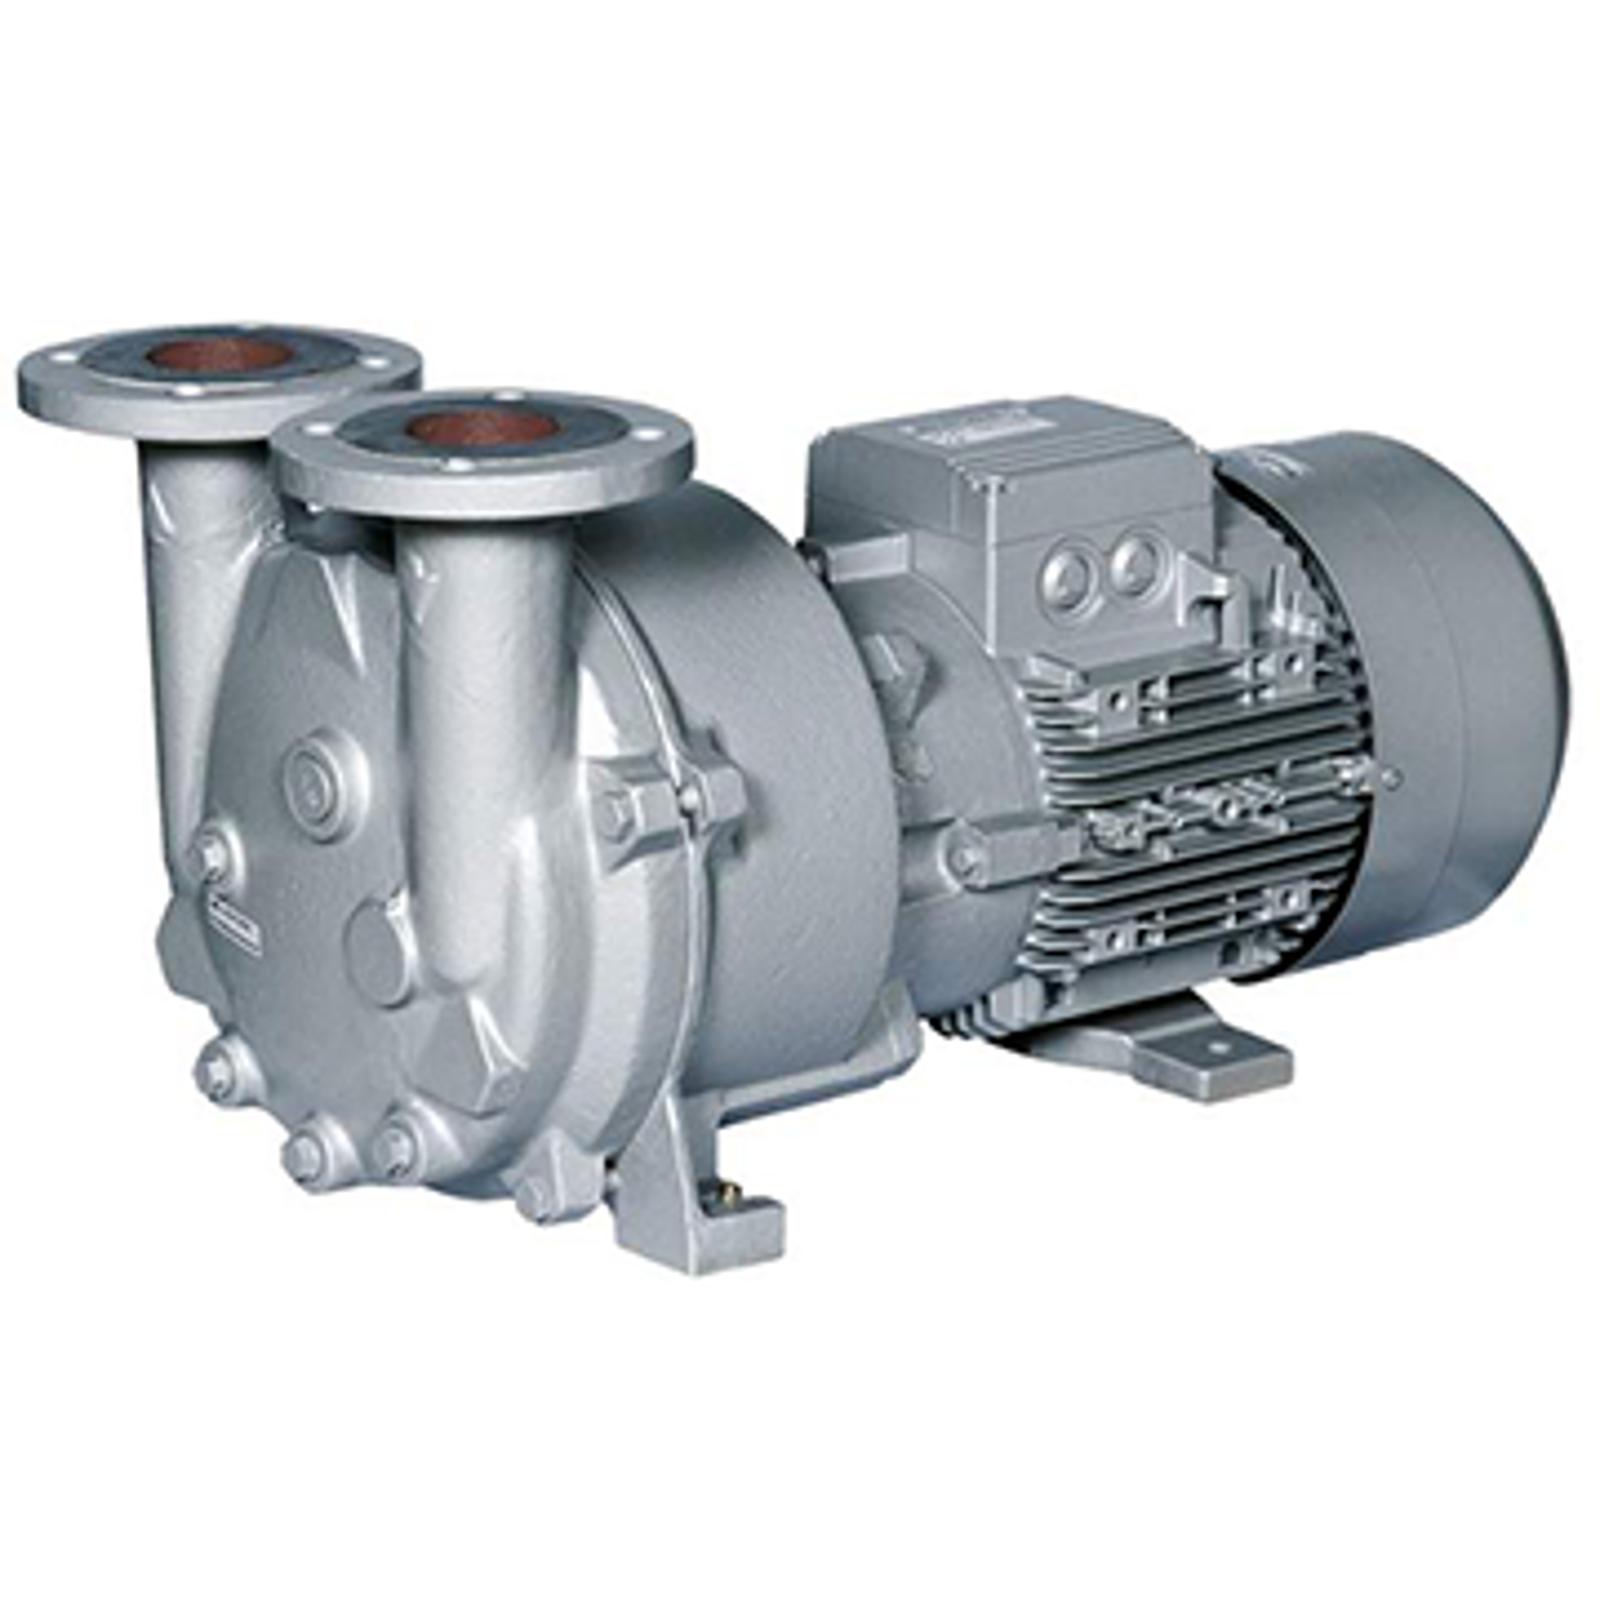
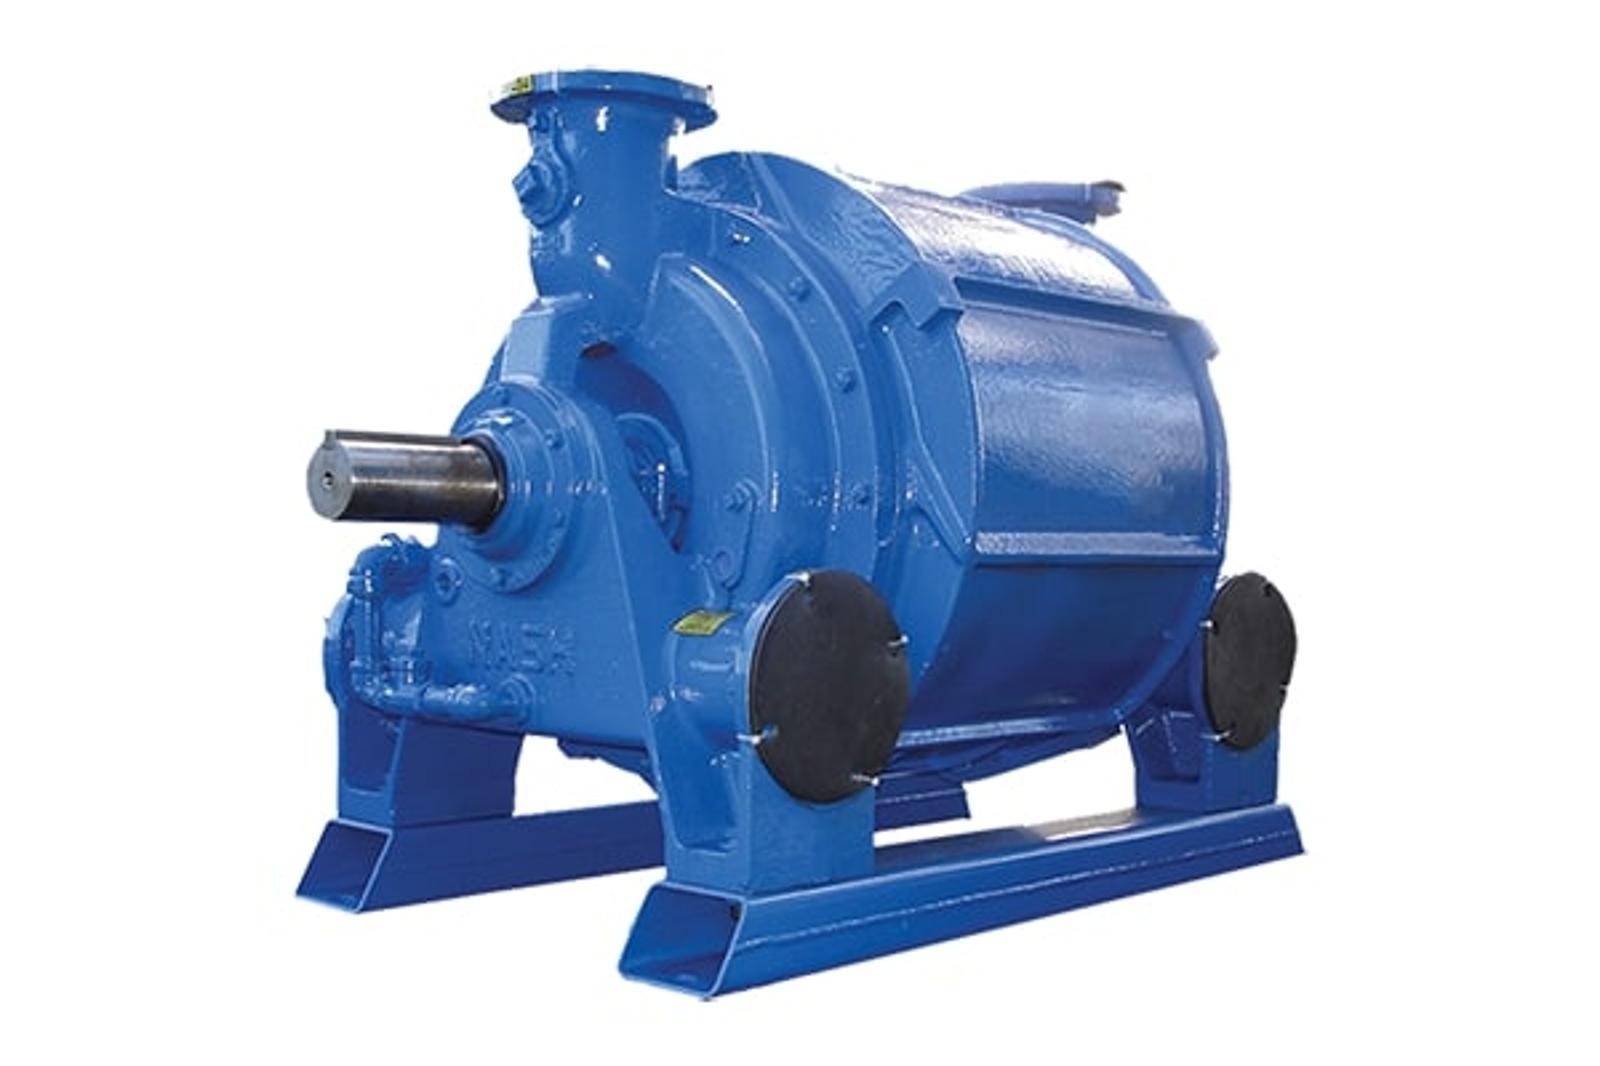
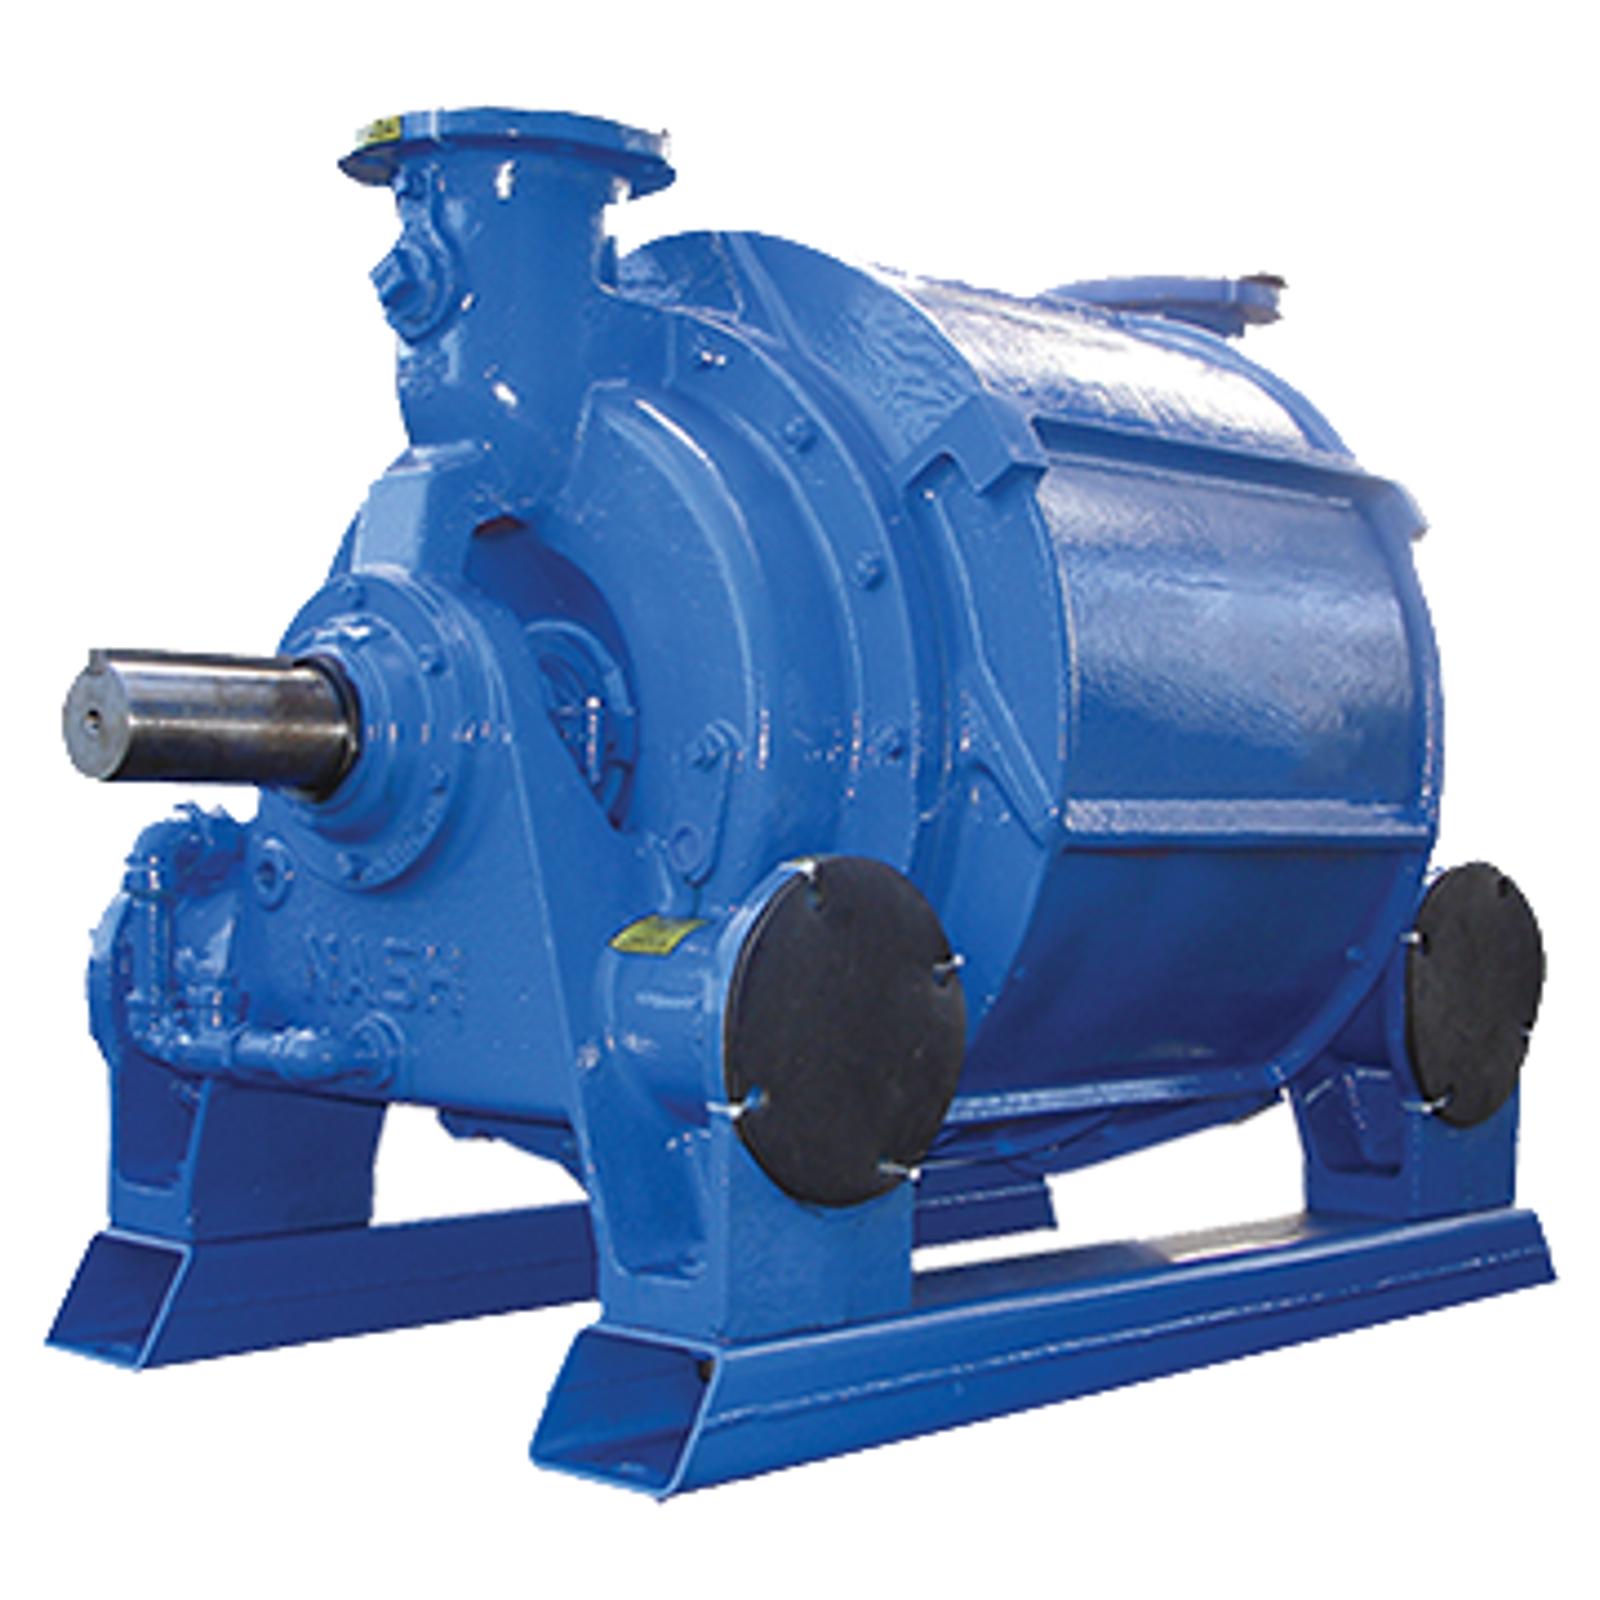
NASH medium to large capacity single stage vacuum pumps are ideal for demanding applications in extremely tough conditions. These heavy-duty pumps are able to serve a wide range of applications, which can typically include dewatering in the paper industry and vacuum filtering in mineral ore processing. Our large capacity pumps are available in a variety of materials including stainless steel, cast iron with some models featuring a polyisoprene lining.
Click the link below to learn more about our large capacity liquid ring vacuum pump.

(Vacuum levels to 0.8in. Hg abs.)
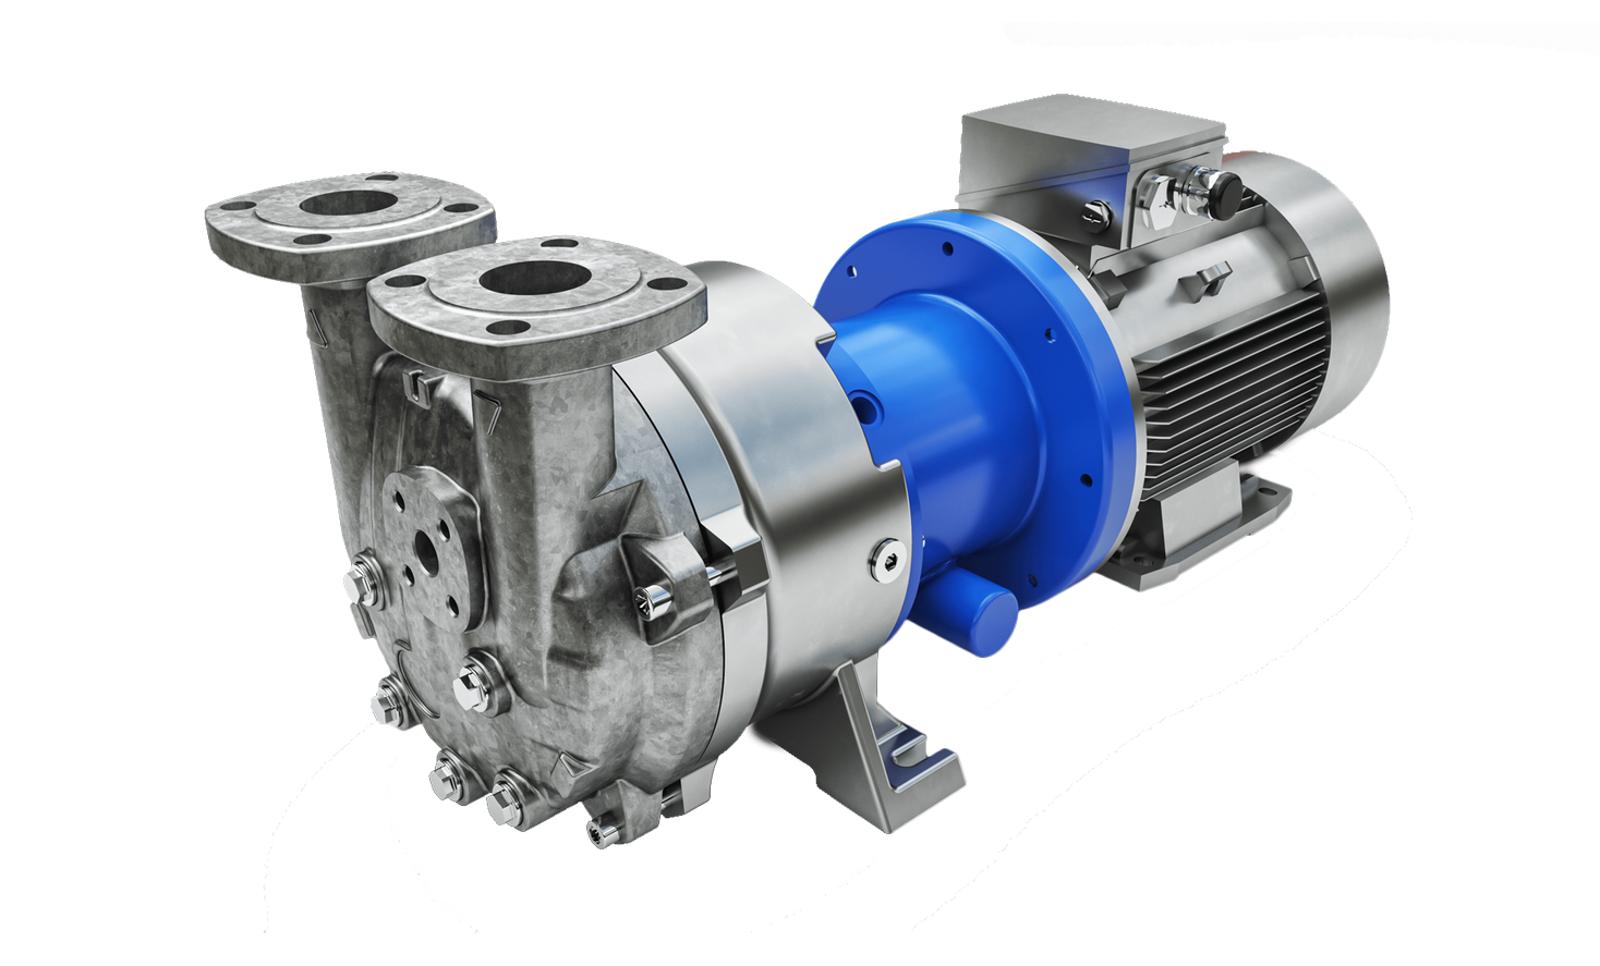
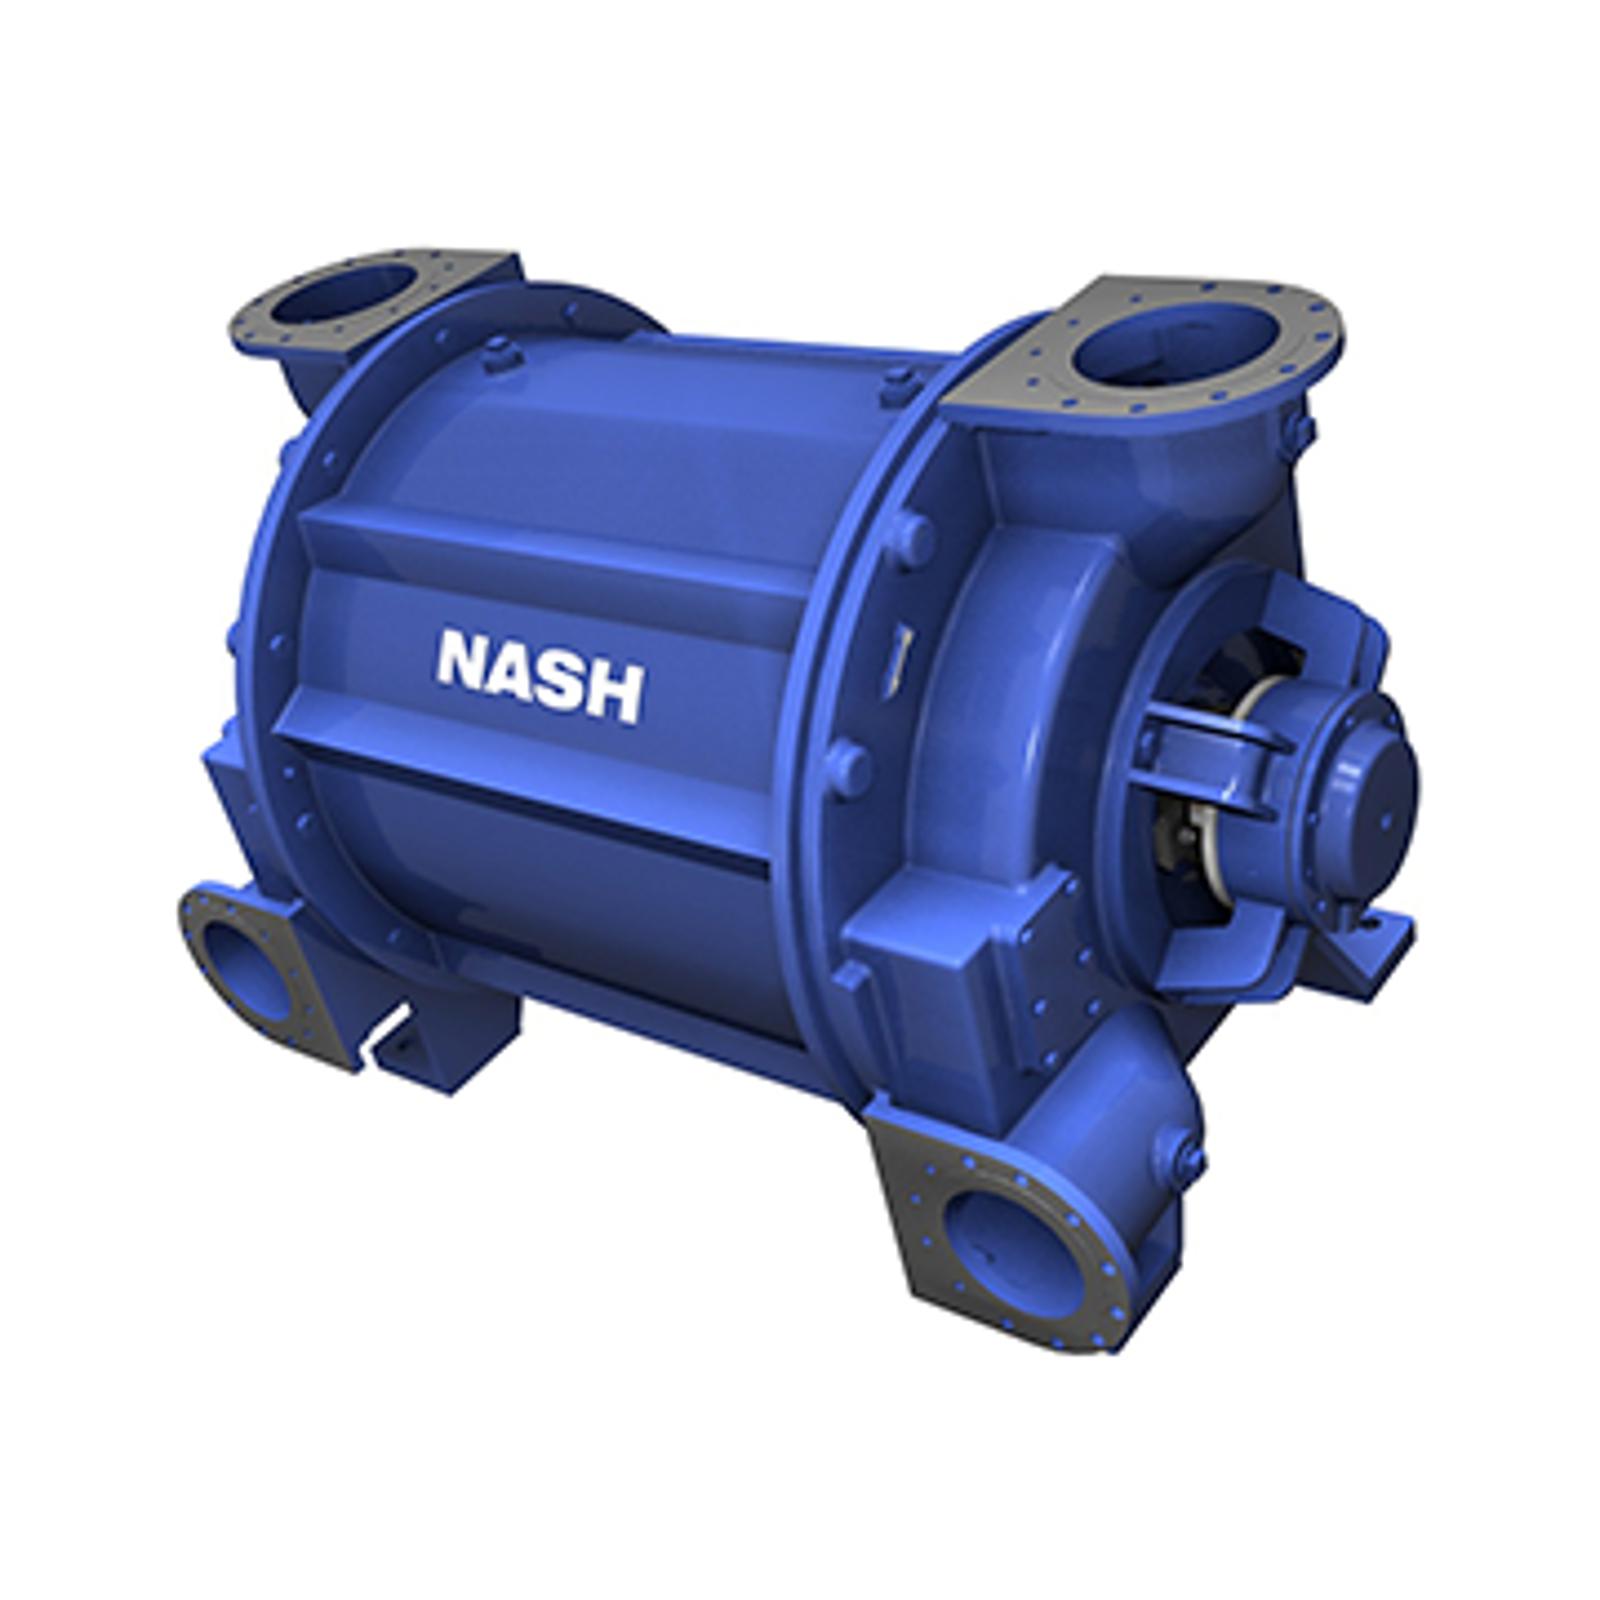
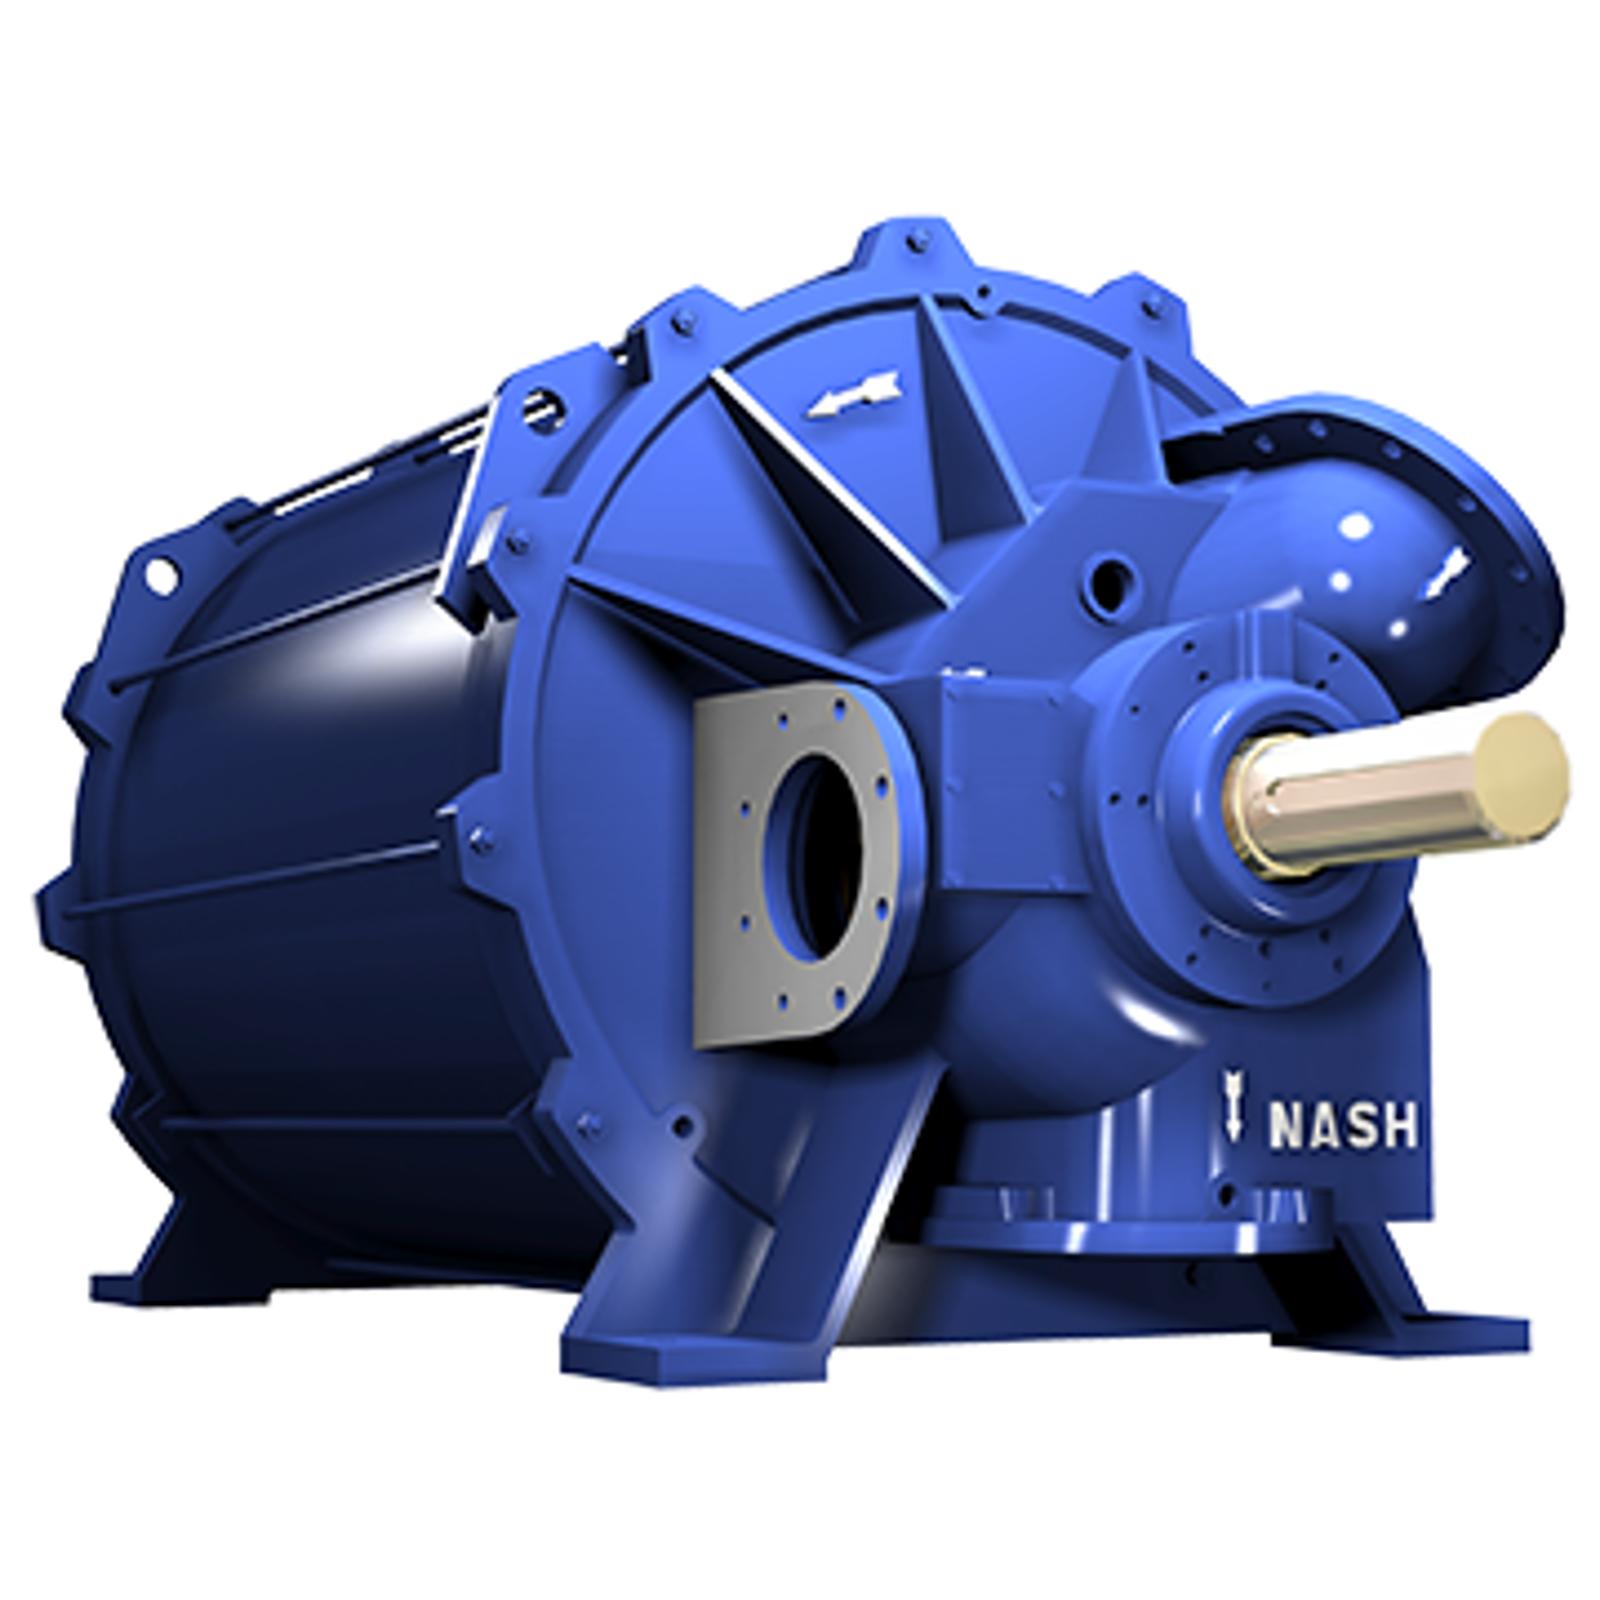
NASH two stage liquid ring vacuum pumps are ideal for a variety of industrial applications and may be combined with ejectors or boosters to form hybrid packages, allowing higher vacuum levels. Nash offers TC two stage liquid ring vacuum pumps, available in ductile iron and stainless steel, and the AT two stage liquid ring vacuum pumps, available in cast iron. Both the TC and AT two stage vacuum pumps feature NASH conical porting.
Click the link below to learn more about our two stage liquid ring vacuum pumps.
NASH liquid ring vacuum pumps can provide reliable vacuum in carbon-capture processes involving wet gas streams and solvent-based systems.
Discover how NASH worked with Bright Renewables to support a municipal heating carbon-capture project and help deliver significant reductions in carbon dioxide emissions.
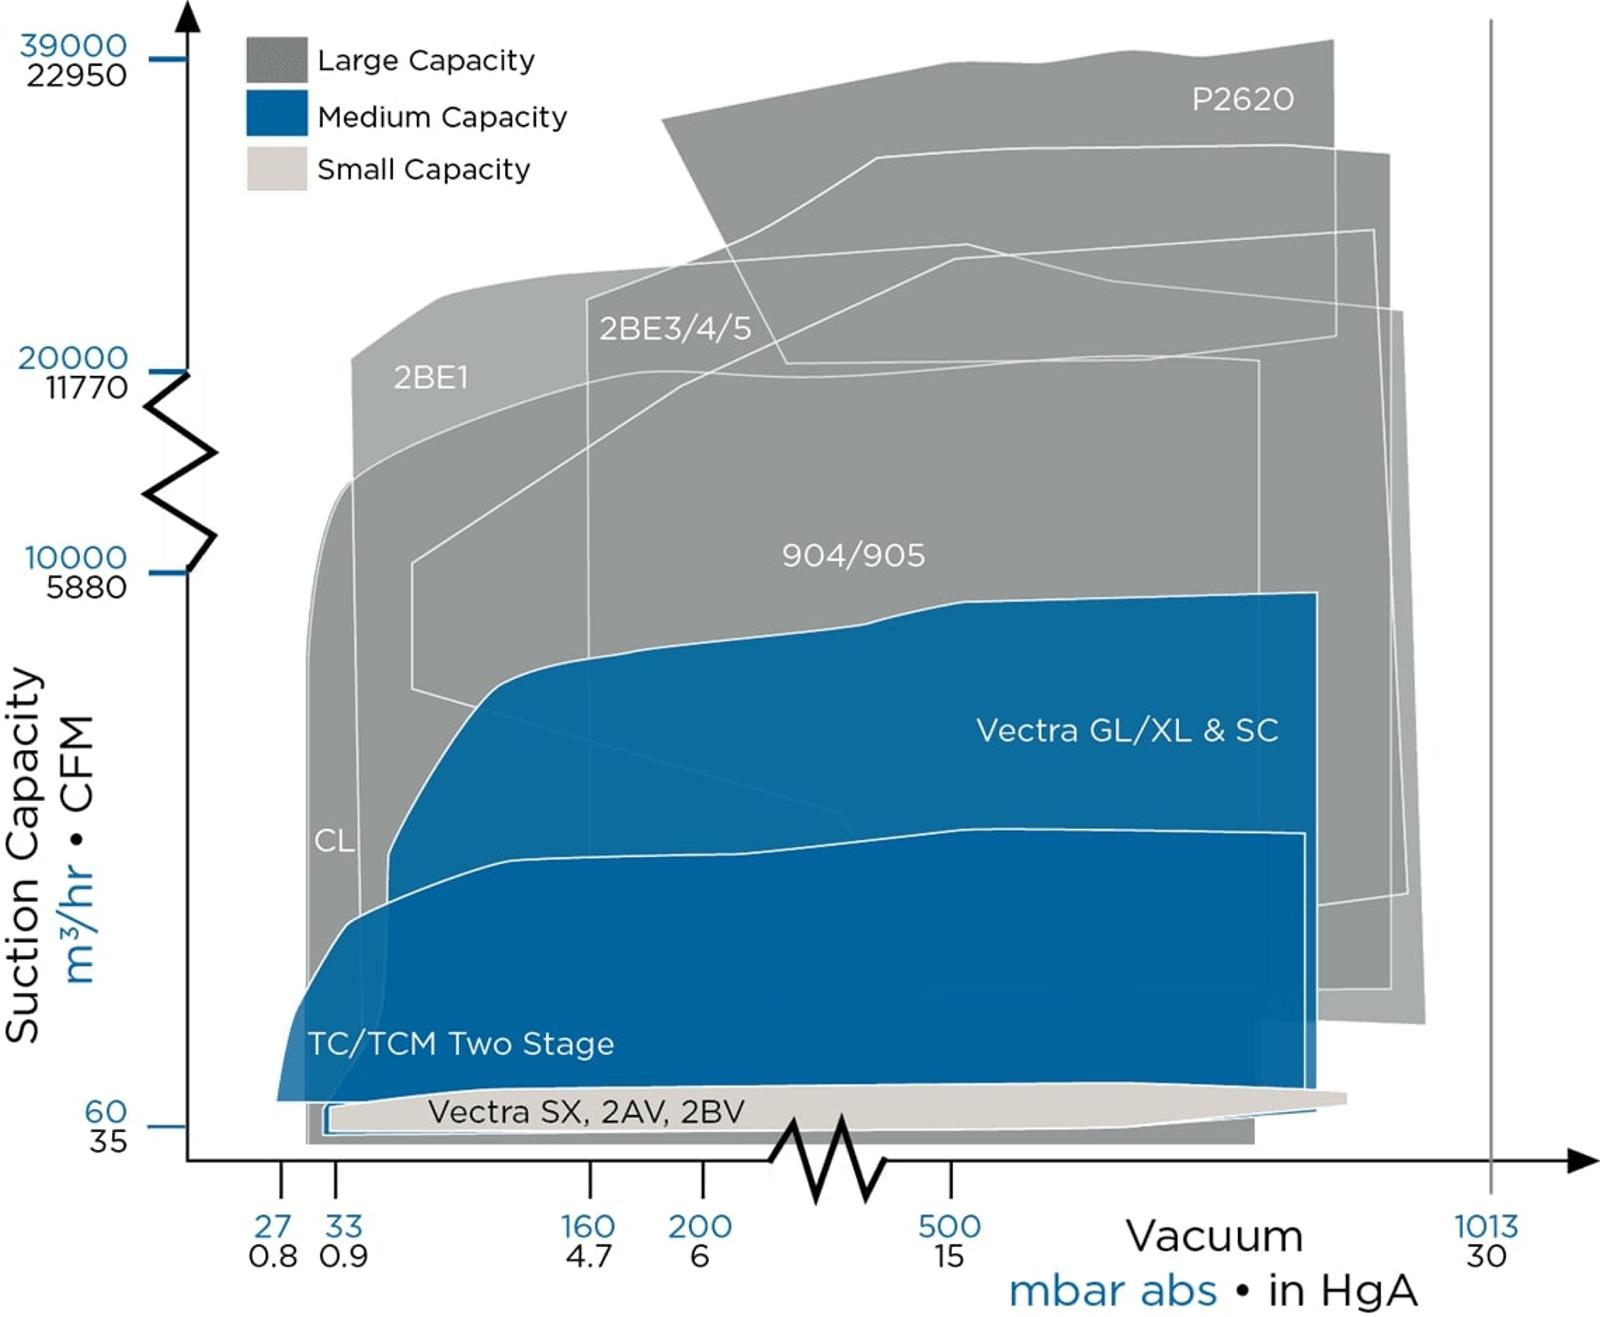
NASH offers liquid ring vacuum pumps across a broad range of capacities and vacuum levels. From compact monoblock pumps to large-capacity continuous-duty equipment and two-stage vacuum systems, each solution can be selected and configured around the required process conditions.
A liquid ring vacuum pump is a rotating positive-displacement pump that uses an eccentrically mounted impeller and a seal liquid to create vacuum. The seal liquid is typically water, although other liquids compatible with the process gas may be used depending on the application.
Unlike many other vacuum technologies, the seal liquid performs an important role in the compression process. It forms the liquid ring that creates the pump's compression chambers while also helping the pump handle wet gases, vapors, and liquid carryover.
During operation, seal liquid is introduced into the pump casing. As the impeller rotates, centrifugal force pushes the liquid outward against the inner wall of the casing, creating a continuously rotating liquid ring.
Because the impeller is positioned eccentrically within the casing, the liquid ring is not concentric with the impeller. This creates spaces of varying volume between the impeller blades and the liquid ring.
As the impeller continues to rotate, the spaces between the blades and the liquid ring increase in volume. This expansion creates vacuum and draws process gas into the pump through the inlet port.
The incoming gas becomes trapped within the spaces between the impeller blades, with the liquid ring acting as a seal between each chamber.
As the impeller moves through its rotation, the eccentric arrangement causes the spaces between the blades and liquid ring to gradually decrease in volume.
This reduction in volume compresses the trapped process gas. Because the compression takes place in direct contact with the seal liquid, liquid ring vacuum pumps are particularly well suited for processes involving saturated gases, condensable vapors, moisture, and liquid carryover.
Once the gas has been compressed, it exits the pump through the discharge port along with a portion of the seal liquid.
Downstream equipment can then separate the process gas from the liquid. Depending on the vacuum system configuration and process requirements, the seal liquid may be discharged after use, partially recirculated, or cooled and fully recirculated through the system.
This simple operating principle helps make liquid ring vacuum pumps a reliable choice for demanding industrial processes. Their ability to tolerate wet and contaminated gas streams can provide an advantage in applications where moisture or condensable vapors may present challenges for other vacuum pump technologies.
NASH liquid ring vacuum pumps are available in small, medium, and large-capacity configurations as well as two-stage designs, allowing a system to be selected around the required vacuum level, capacity, process gas, seal liquid, and operating conditions.
Correct pump selection requires more than matching horsepower or nominal suction capacity. Important process factors include:
Determine the normal operating pressure, maximum required vacuum, and whether the process requires a single-stage, two-stage, or hybrid vacuum system.
Establish the required gas flow at the actual inlet pressure and temperature. Pump capacity should be based on process conditions rather than free-air displacement alone.
Identify the gases, condensable vapors, moisture, chemicals, solids, and expected liquid carryover entering the pump.
Confirm which seal liquid is compatible with the process. Water is commonly used, but another process-compatible liquid may be required. Seal-liquid temperature, flow, and vapor pressure should be considered during pump sizing.
Select cast iron, stainless steel, elastomer-lined, or other construction based on corrosion, erosion, temperature, and process-compatibility requirements.
Mechanical seals may be appropriate for general applications, while magnetic-drive pumps can provide hermetically sealed operation for processes requiring enhanced containment.
The pump may use once-through seal liquid, partial recirculation, or total recirculation. The correct arrangement depends on utility availability, discharge requirements, contamination risk, and operating cost objectives.
Back pressure, separator design, exhaust treatment, and downstream process requirements can affect pump performance and system configuration.
Available space, motor requirements, controls, redundancy, ambient conditions, hazardous-area classifications, and maintenance access should be evaluated before final selection.
Because vacuum-pump performance depends on the complete process, published data should be used for preliminary comparison only. Consult a NASH engineer for final pump sizing and system design.
A liquid ring vacuum pump is a rotating positive-displacement pump that uses a liquid ring to draw in and compress process gas. The operating liquid is commonly water, although another compatible liquid may be used when required by the process.